Replacement and OEM screw barrel sets for injection molding machines — built to your machine brand, screw diameter and resin. Standard range Ø12–300 mm with L/D 10–26, nitrided or bimetallic.
The injection screw barrel is the plasticating unit of an injection molding machine. The screw rotates inside the barrel to convey, compress, melt and homogenize the resin, then acts as a plunger to inject the melt into the mould.
Because shot size, cycle time and melt quality all depend on this unit, wear in the screw flights or barrel bore shows up directly as short shots, black specks, colour streaks and unstable dimensions in finished parts.
We build complete matched sets — screw and barrel machined as a pair — for machine brands including Engel, Arburg, Boy, Demag, JSW, Toshiba, Sumitomo, Haitian and LG. Send us the machine model or the worn sample and we confirm the geometry before production.
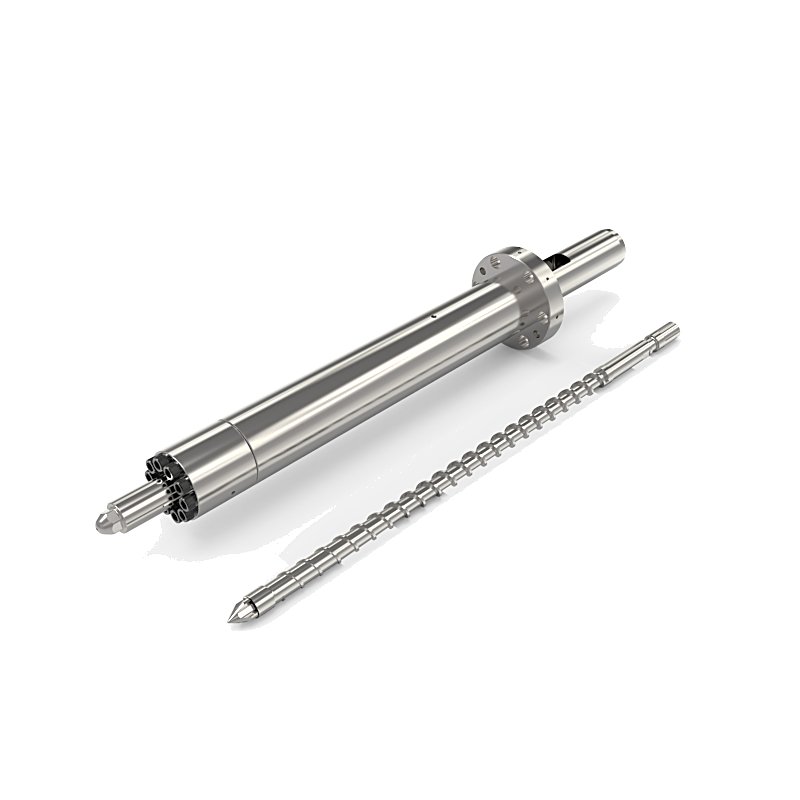
Three-zone design for PE, PP, PS and ABS. The default choice for commodity resin moulding.
Separates melt from unmelted solid to raise output and lower melt temperature on polyolefins.
Distributive mixing elements for colour masterbatch, additive blending and colour uniformity.
Low-shear, corrosion-resistant geometry with chrome or bimetallic protection for heat-sensitive PVC.
Low-compression design for optical-grade and engineering resin with tight melt temperature control.
High-compression design for PET preform and bottle-grade resin with low acetaldehyde generation.
Optimised for thin-wall packaging and fast-cycle moulding where plasticating rate is the bottleneck.
Vented barrel with degassing port for hygroscopic or volatile-generating materials.
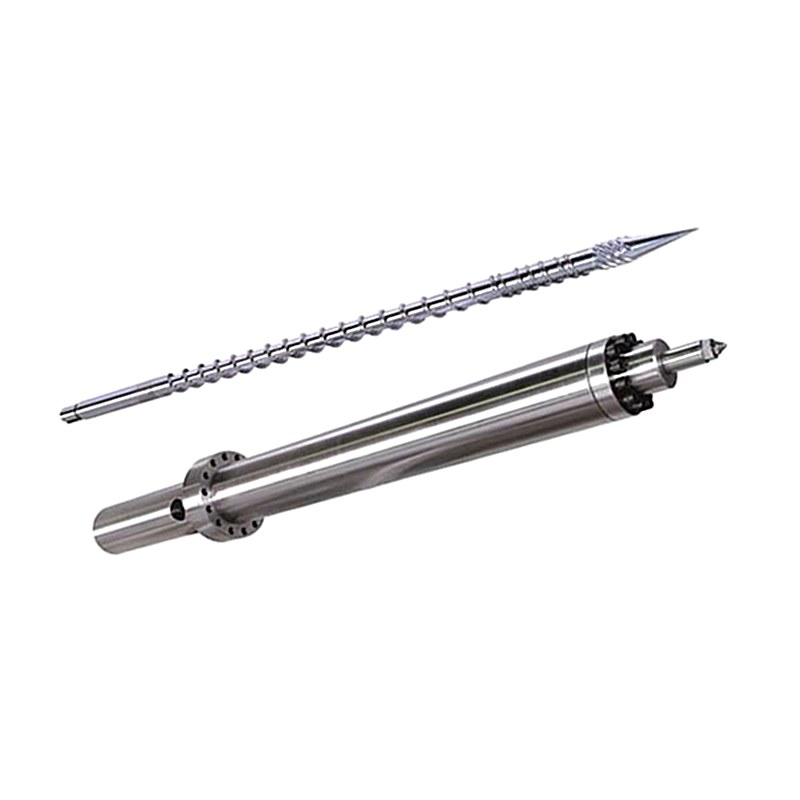
Complete matched set for 90–450 t injection moulding machines, nitrided or bimetallic.
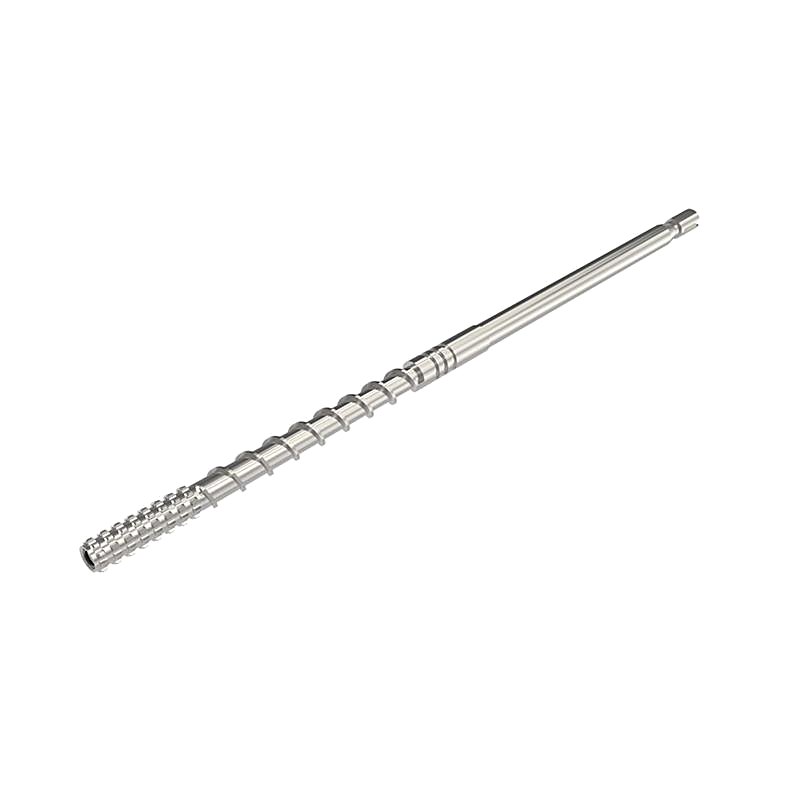
High-compression PET screw with barrier tips, low acetaldehyde generation for bottle-grade preforms.
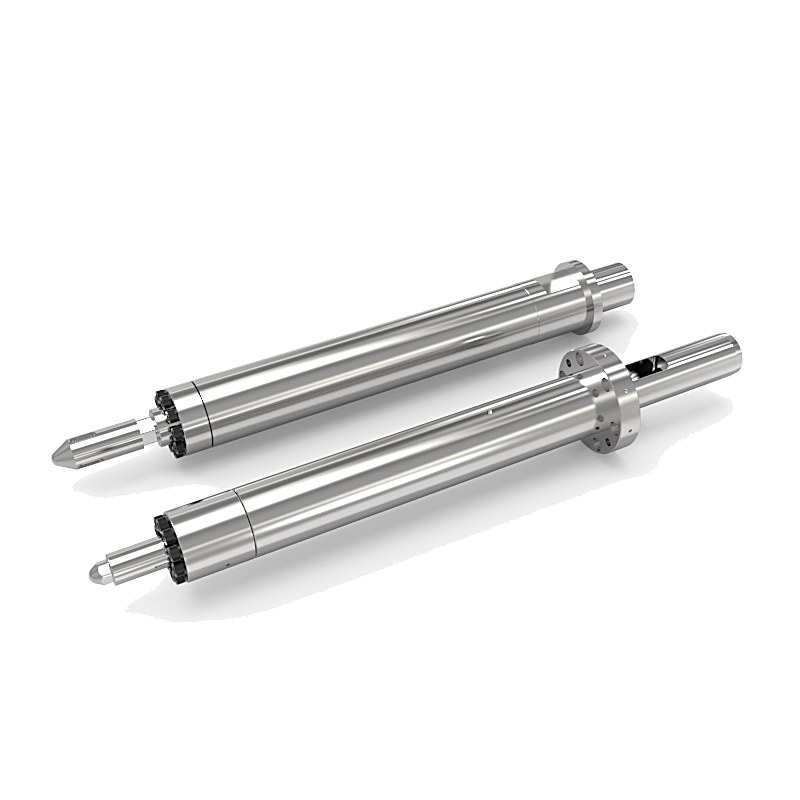
Centrifugally cast 2–5 mm alloy lining for glass-filled and corrosive resins.
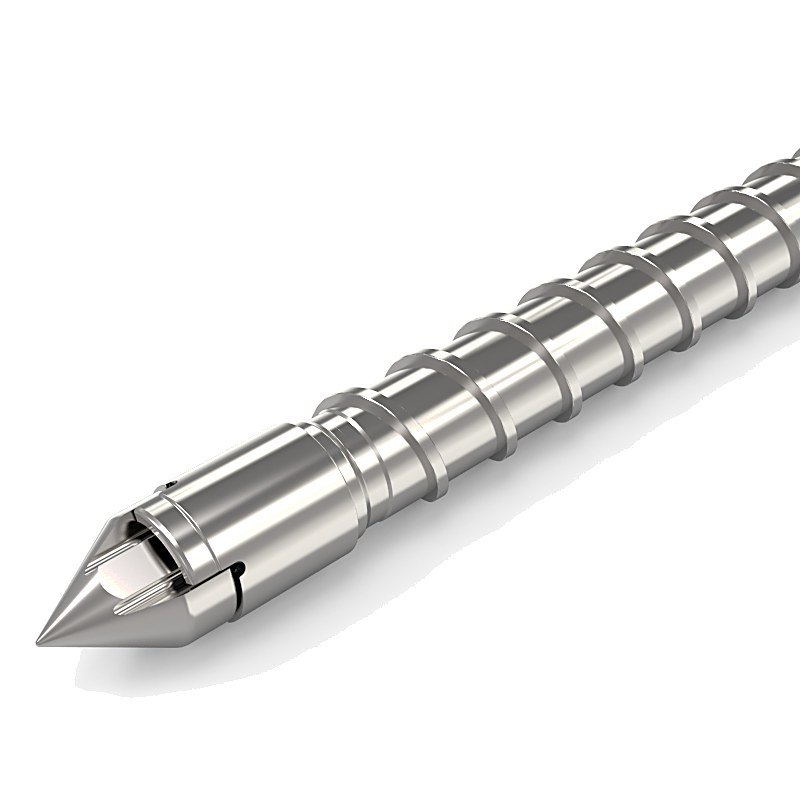
Three-zone GP screw for PE, PP, PS and ABS with polished flight profile.
Low-shear PVC screw with corrosion-protected barrel for pipe fitting and valve injection.
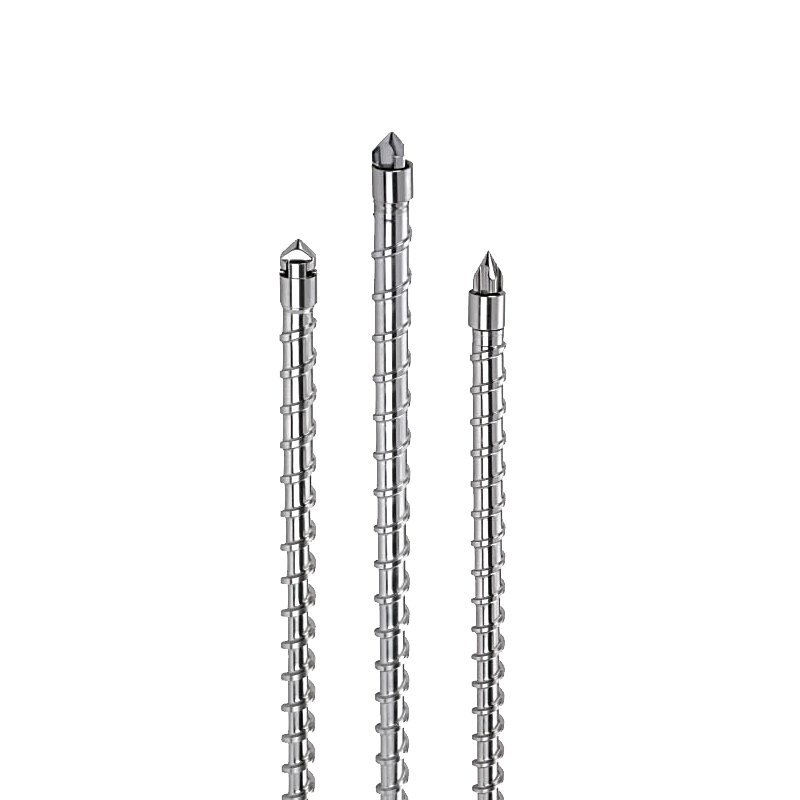
Low-degradation screw barrel for polycarbonate and acrylic optical and lighting parts.
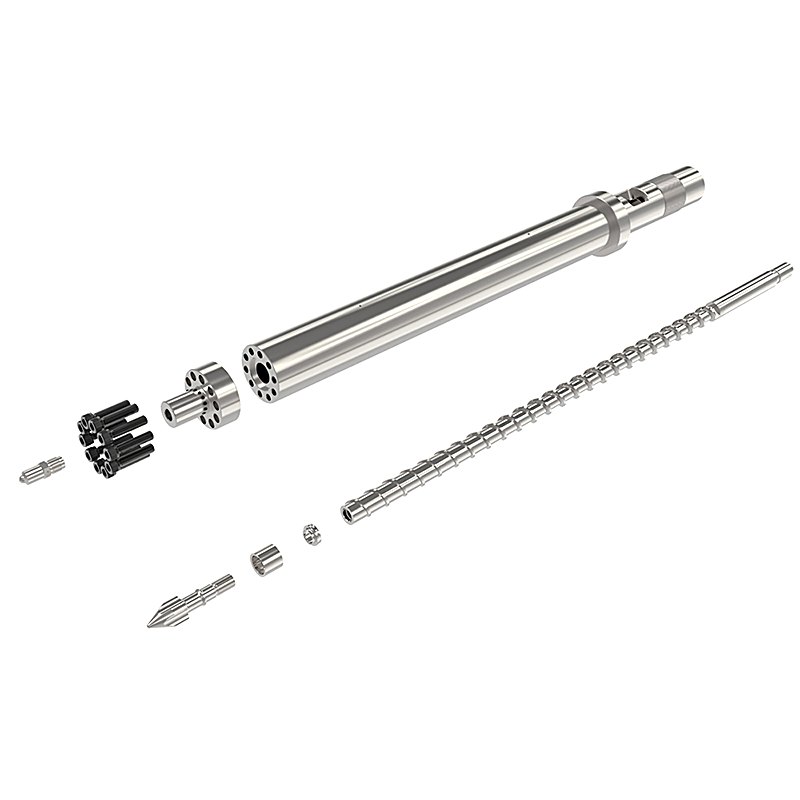
High-throughput screw barrel for thin-wall food packaging and fast-cycle moulding.
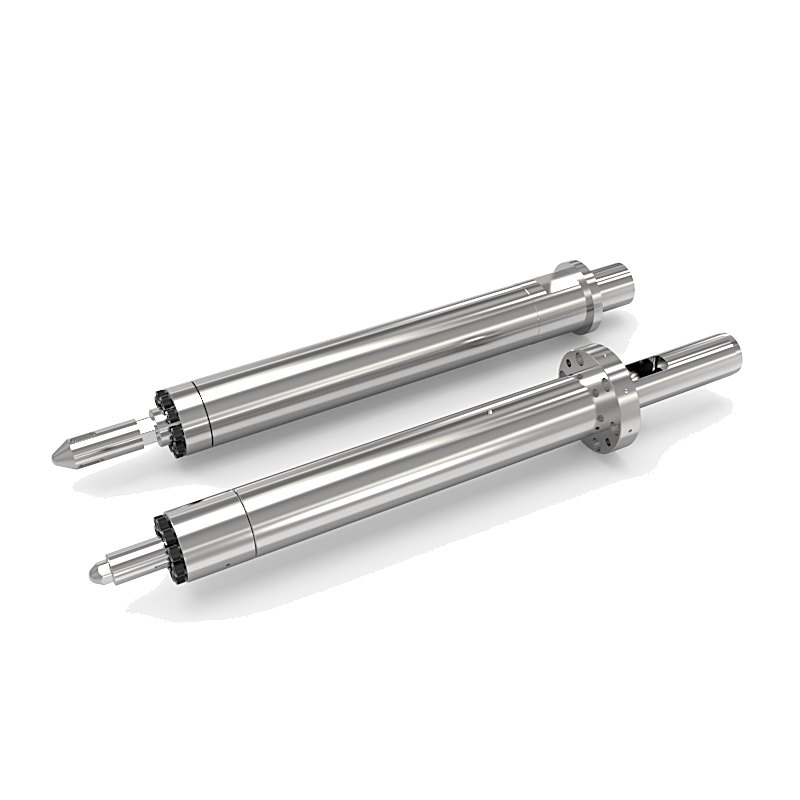
Bimetallic barrel and hardened screw package for 30–50% glass-filled PA6 / PA66.
New models are added regularly — or send your drawing or worn sample for a custom build.
Standard ranges shown below. Non-standard sizes and custom geometry are built to your drawing or sample.
| Item | Specification |
|---|---|
| Screw Diameter | Ø12 – Ø300 mm |
| L/D Ratio | 10 – 26 (custom on request) |
| Barrel Type | Solid barrel, vented barrel, bimetallic-lined barrel |
| Base Material | 38CrMoAlA, 42CrMo, 40Cr, stainless steel |
| Nitriding Depth | 0.4 – 0.7 mm, surface hardness HV 900–1100 |
| Bimetallic Layer | 2 – 5 mm alloy lining for abrasive / corrosive resin |
| Machining Tolerance | ±0.02 mm on critical fits |
| Straightness | ≤0.015 mm/m after finish grinding |
| Machine Brands | Engel, Arburg, Boy, Demag, JSW, Toshiba, Sumitomo, Haitian, LG and others |
| Lead Time | Confirmed with quotation depending on size and treatment |
Material and treatment are selected by the resin you process, filler content and expected service life.
Standard choice for general-purpose resin. Gas nitriding gives a hard, wear-resistant case with a tough core.
Through-hardened alloy steel for higher torque and shock loads on larger machines.
2–5 mm cast alloy layer for glass-filled, flame-retardant or recycled material. Service life far beyond nitrided.
For corrosive resin (PVC, fluoropolymers) and food or medical-grade applications.
Optional surface treatment on flights for additional abrasion protection.
Case depth 0.5–0.8 mm at HV 900–1020, verified on every batch.
Common problems we help injection and extrusion plants solve — and how a matched screw barrel fixes them.
Part weight drifts and short shots appear as clearance between screw and barrel grows.
Matched set restores clearance and stabilises shot volume.Degraded resin hangs on worn flight surfaces and carbonises into the melt.
Fresh surface plus optimised geometry removes dead zones.Worn feed section reduces plasticating rate, forcing a longer cycle to fill the part.
Correct compression ratio restores original plasticating capacity.Material accumulates in worn crevices and bleeds into the next colour.
Smooth, correctly finished surfaces cut purge time substantially.The motor works harder to push melt through degraded geometry.
Properly matched clearance lowers torque and energy draw.Downtime waiting for a replacement set costs more than the part itself.
3,000–5,000 sets a year of capacity keeps standard sizes in production.We review your drawing, machine model or reverse-engineer the worn sample, then confirm the geometry with you.
Bar stock from certified mills, with chemical composition and ultrasonic inspection before cutting.
Turning and milling of barrel bore and screw blank with allowance for heat treatment.
Gas nitriding or bimetallic casting, followed by hardness verification on test coupons.
CNC thread grinding and bore finishing to reach final tolerance and straightness.
Screw and barrel fitted, clearance checked, dimensions recorded, then rust-protected and packed.
Interior trim, bumpers, lamp housings and under-hood components.
Housings, panels and structural parts for white goods and small appliances.
Thin-wall containers, caps, closures and food-grade packaging.
Syringes, test tubes and consumables requiring clean, stable melt.
Connectors, enclosures and precision components with tight tolerances.
PPR, PVC and PE fittings for plumbing and irrigation systems.
“We sent a worn set from our Engel machine instead of a drawing. The replacement fitted straight in and shot weight is stable again.”
Maintenance ManagerAutomotive parts moulder, Europe“Colour change used to take most of a shift. With the new bimetallic set on our glass-filled material it is much faster.”
Production SupervisorAppliance components manufacturer“The drawing was confirmed before production, so there was no surprise at installation. That saved us a machine stoppage.”
Purchasing LeadPackaging converter, South AmericaYes. Send the worn screw and barrel, or just the machine model and screw diameter with basic dimensions. We reverse-engineer the geometry and send a confirmation drawing for your approval before production starts.
We regularly build sets for Engel, Arburg, Boy, Demag, JSW, Toshiba, Sumitomo, Haitian and LG, among others. For less common brands, send the model plate and we will confirm whether we have the geometry on file or need a sample.
Nitrided is sufficient for unfilled commodity resin. If you run glass-filled, mineral-filled, flame-retardant or recycled material, a bimetallic lining gives substantially longer service life and is usually cheaper per running hour.
It depends on diameter, length and heat treatment. Because machining, nitriding and finishing are done in-house, we confirm a realistic schedule together with the quotation.
Both. A matched set is recommended because screw and barrel wear together — replacing only one leaves the worn part to accelerate wear on the new one.
Rust-protected, fixed inside a wooden case with clear marking, suitable for sea, air and express shipment.
Send the drawing, machine model or worn sample — we confirm the geometry and quote within one working day.
Tell us the machine model, screw diameter and material you process — we will reply with a matched solution and quotation.
Or write directly to info@xiwangindustry.com · WhatsApp +86-13503734287
On unfilled commodity resin a correctly nitrided set typically runs for several years. On glass-filled or flame-retardant grades the same geometry may last a fraction of that unless it is built bimetallic. Rather than quote a number we do not control, we ask for your resin, filler percentage and running hours, then select the metallurgy that makes the interval predictable.
Yes, and this is one of the most useful upgrades available. We change the base steel or move to a bimetallic construction, adjust the compression ratio and check-valve geometry for the new melt behaviour, and rebuild the barrel to match. Most customers gain several times the previous service life.
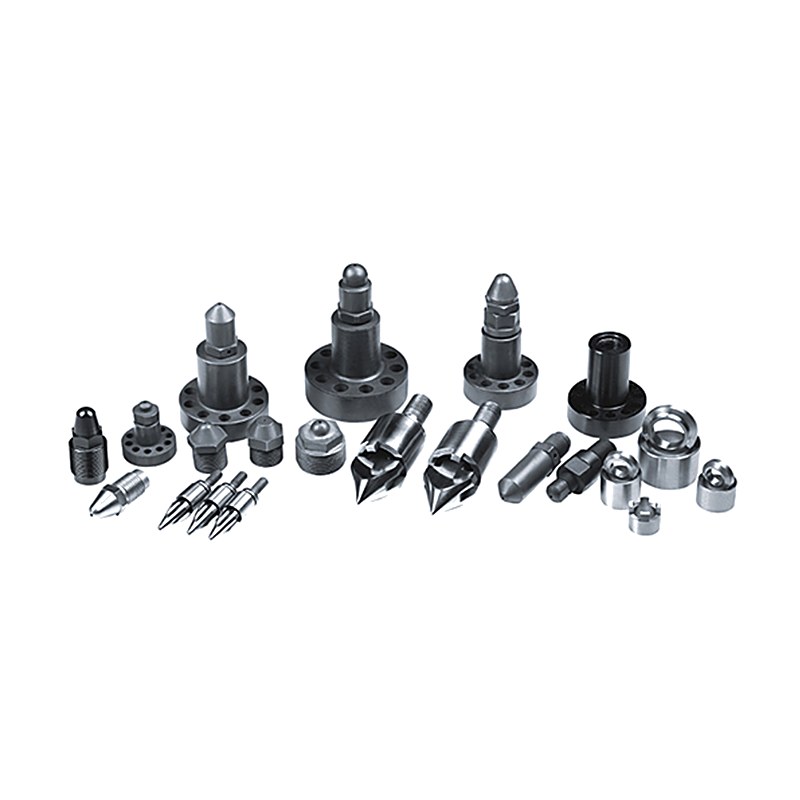
Yes. Tip, check ring and seat can be rebuilt or supplied new with the screw, matched to the same wear specification so no component becomes the weak link.
Tell us your machine model, drawing or worn sample — we reply with a matching proposal and quotation within one business day.