Low-degradation screw barrel for polycarbonate and acrylic optical and lighting parts. Machined in our own Henan workshop — to your drawing, or reverse-engineered from your worn parts.
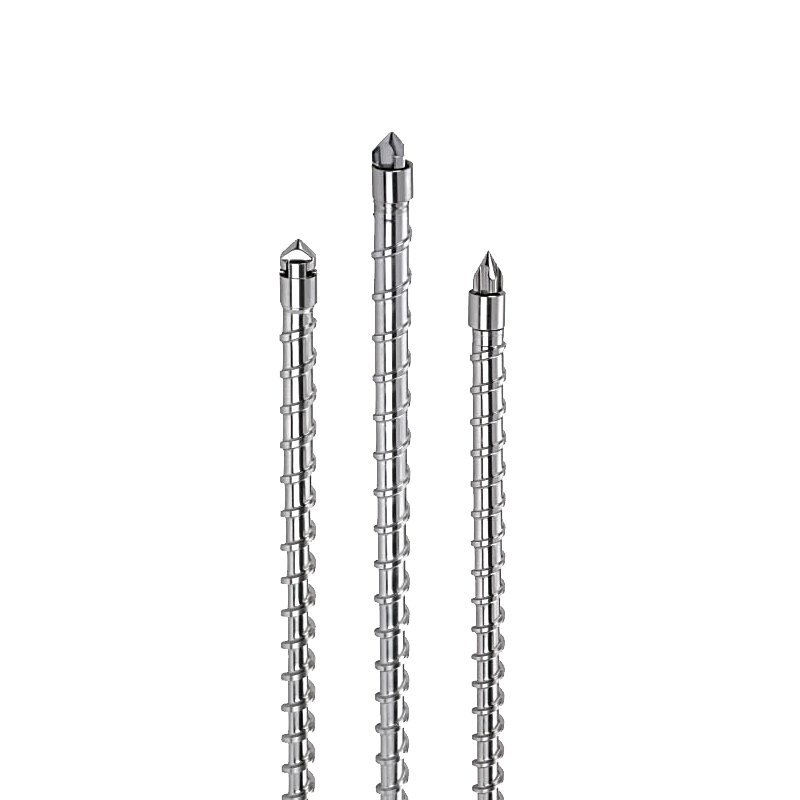
PC and PMMA hold their value only while the melt stays clean: streaks, silver marks and yellowing all trace back to shear heat and long residence. Our optical-grade screw runs a moderate compression profile with a generous metering zone and a mirror-polished channel.
Supplied for lenses, light guides, headlamp lenses and optical panels. We can also match your existing barrel bore and deliver a screw only if the barrel still measures within tolerance.
Quote within one business day. We reply with a matching proposal, delivery date and price — no generic catalogue PDF.
Standard range shown. Every dimension below can be changed to your machine, resin and output — custom manufacturing is our daily business.
| Screw diameter | Ø30–130 mm |
|---|---|
| L/D ratio | 20–24 |
| Compression ratio | 2.2–2.4, gentle transition |
| Channel finish | Mirror polished, Ra ≤ 0.2 |
| Material | 38CrMoAlA gas nitrided HV 900–1020 |
| Barrel bore | Honed Ra 0.4, straightness ≤ 0.015 mm |
| Lead time | 30–40 days |
The honest answer depends on your resin, not on price. Here is how we advise customers.
| Gas Nitrided (38CrMoAlA) | Bimetallic Alloy Lining | |
|---|---|---|
| Best for | Unfilled PE, PP, PS, ABS, virgin PVC | Glass-filled, mineral-filled, recycled, corrosive |
| Surface hardness | HV 900–1020, depth 0.45–0.7 mm | Alloy layer 2–5 mm, metallurgically bonded |
| Typical service life | Baseline | 3–5× baseline on abrasive resin |
| Cost | Lower | Higher, recovered through fewer stoppages |
| Certification | MTC with heat number | MTC + hardness records, third-party on request |
Mostly by geometry and finish: a gentle compression transition, a long metering zone and a mirror-polished channel keep the melt below degradation. Drying practice on your side matters just as much — we will tell you that too.
Yes — the same screw family covers PC/ABS; we adjust the compression ratio slightly for the blend ratio you run.
Not usually. Unfilled PC and PMMA are mild to steel; nitrided is sufficient. Switch to bimetallic only if you run filled or flame-retardant grades.
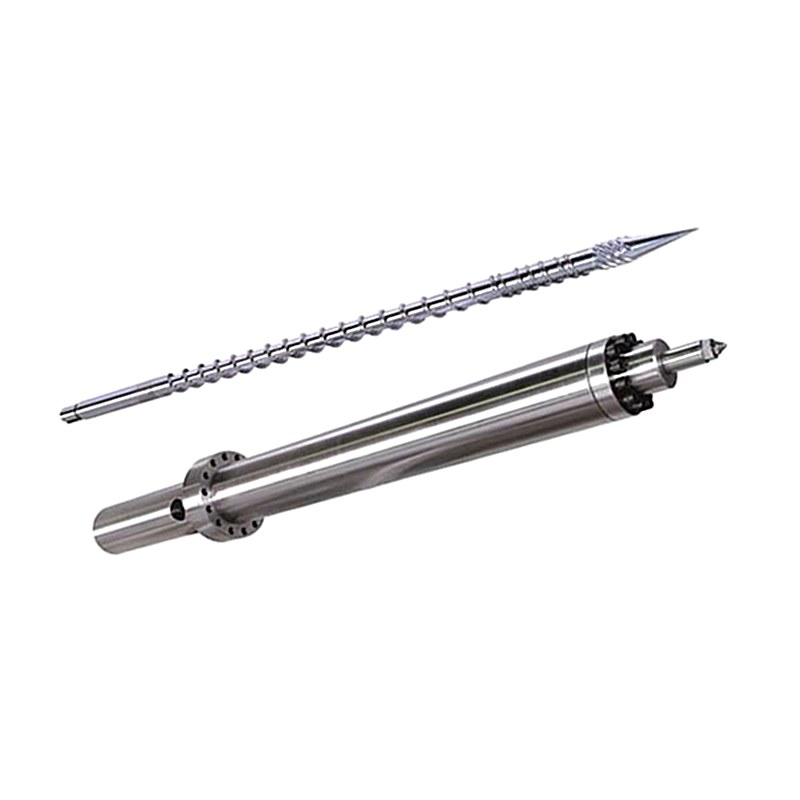
Complete matched set for 90–450 t injection moulding machines, nitrided or bimetallic.
View Details →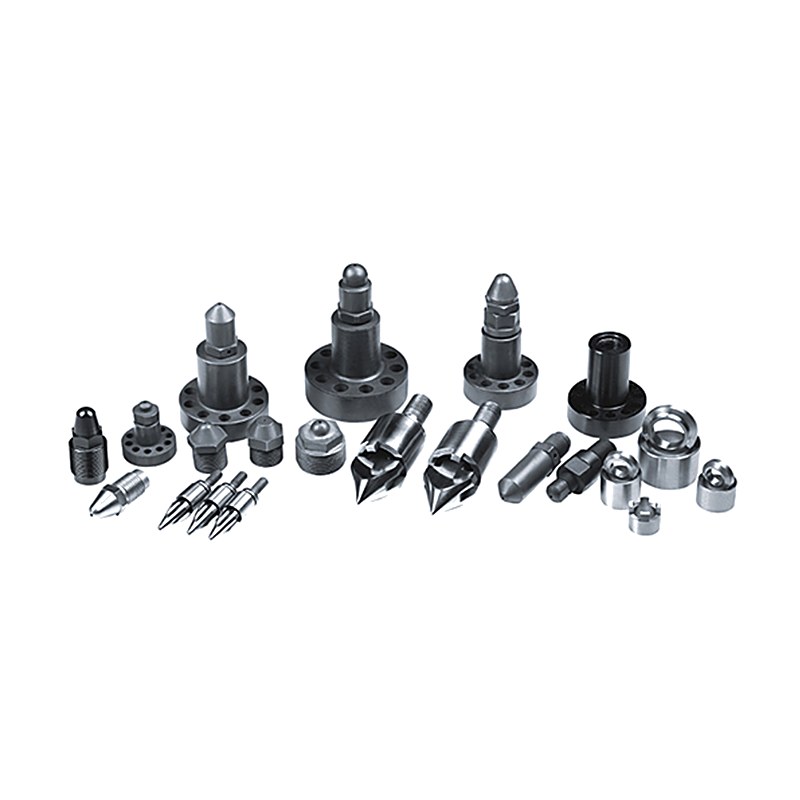
High-compression PET screw with barrier tips, low acetaldehyde generation for bottle-grade preforms.
View Details →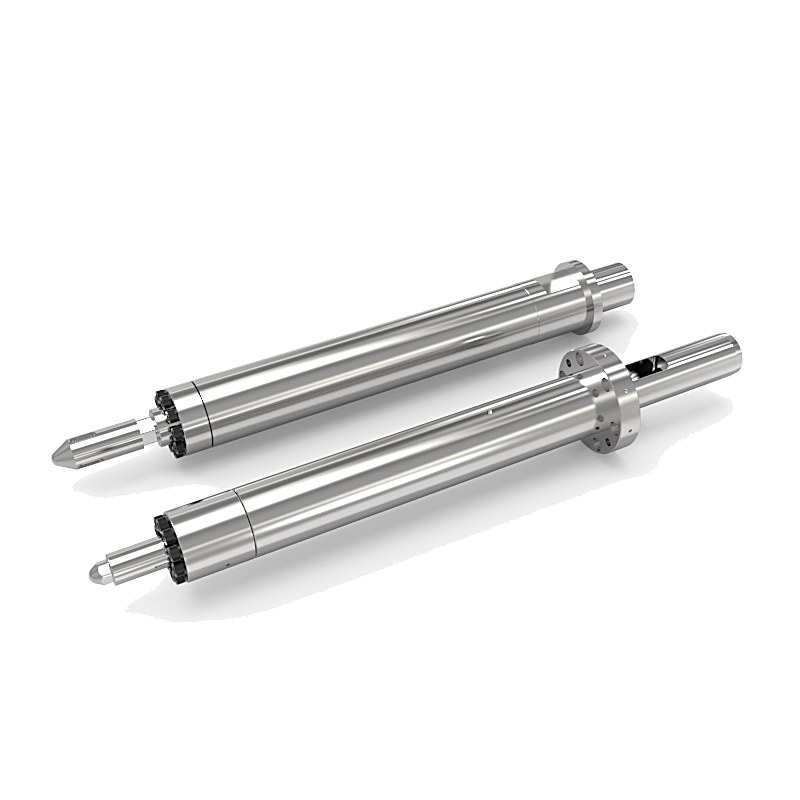
Centrifugally cast 2–5 mm alloy lining for glass-filled and corrosive resins.
View Details →Send your machine model, drawing or worn sample — we reply with a matching proposal and quotation within one business day.