High-compression PET screw with barrier tips, low acetaldehyde generation for bottle-grade preforms. Machined in our own Henan workshop — to your drawing, or reverse-engineered from your worn parts.
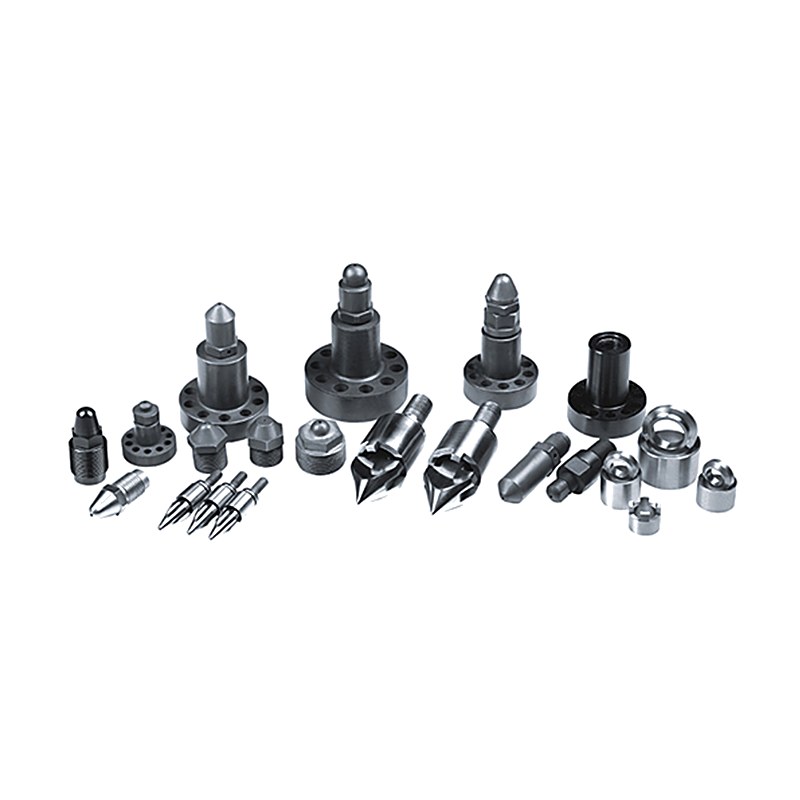
PET punishes a poorly designed screw: acetaldehyde climbs, preforms yellow and the IV drops. Our preform screws use a barrier flight with a dedicated mixing section so the melt stays below the degradation threshold at high throughput.
We build these for 24 to 96 cavity preform systems. Tell us your cycle time and shot weight and we size the compression ratio and L/D to keep the melt temperature flat across the whole shot.
Quote within one business day. We reply with a matching proposal, delivery date and price — no generic catalogue PDF.
Standard range shown. Every dimension below can be changed to your machine, resin and output — custom manufacturing is our daily business.
| Screw diameter | Ø30–120 mm |
|---|---|
| L/D ratio | 20–27 for PET |
| Compression ratio | 2.0–2.6, tuned to IV |
| Screw design | Barrier + mixing head |
| Material | 38CrMoAlA nitrided / bimetallic for recycled PET |
| Surface | Polished flights, chrome option |
| Lead time | 30–40 days after drawing approval |
The honest answer depends on your resin, not on price. Here is how we advise customers.
| Gas Nitrided (38CrMoAlA) | Bimetallic Alloy Lining | |
|---|---|---|
| Best for | Unfilled PE, PP, PS, ABS, virgin PVC | Glass-filled, mineral-filled, recycled, corrosive |
| Surface hardness | HV 900–1020, depth 0.45–0.7 mm | Alloy layer 2–5 mm, metallurgically bonded |
| Typical service life | Baseline | 3–5× baseline on abrasive resin |
| Cost | Lower | Higher, recovered through fewer stoppages |
| Certification | MTC with heat number | MTC + hardness records, third-party on request |
Yes, but specify it. rPET carries more contamination and fines, so we recommend a bimetallic barrel and a slightly deeper feed channel. Say 'rPET' in your enquiry and we allow for it.
Yes. If your barrel is still within tolerance we can machine a screw to match the existing bore — send the bore measurement or the barrel itself.
By keeping shear low: barrier flight, correct compression ratio, polished channels and a melt temperature we verify against your resin's datasheet before we finalise the drawing.
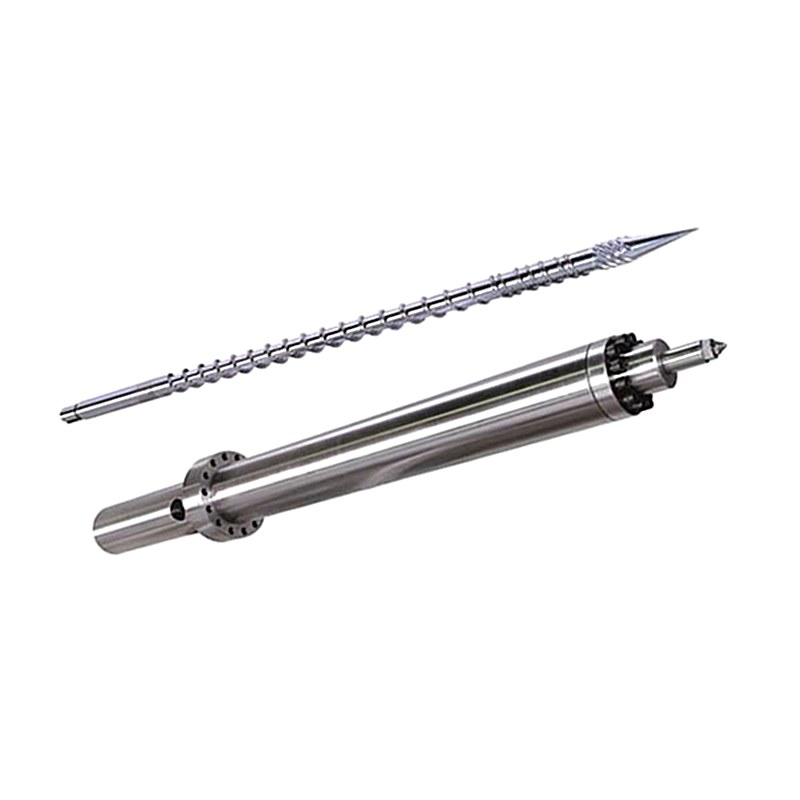
Complete matched set for 90–450 t injection moulding machines, nitrided or bimetallic.
View Details →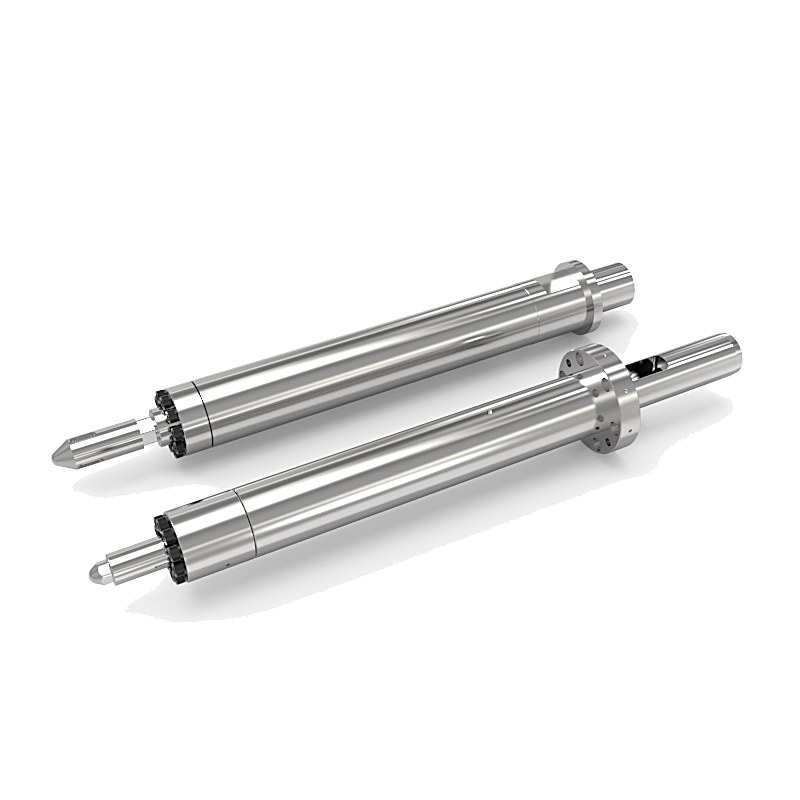
Centrifugally cast 2–5 mm alloy lining for glass-filled and corrosive resins.
View Details →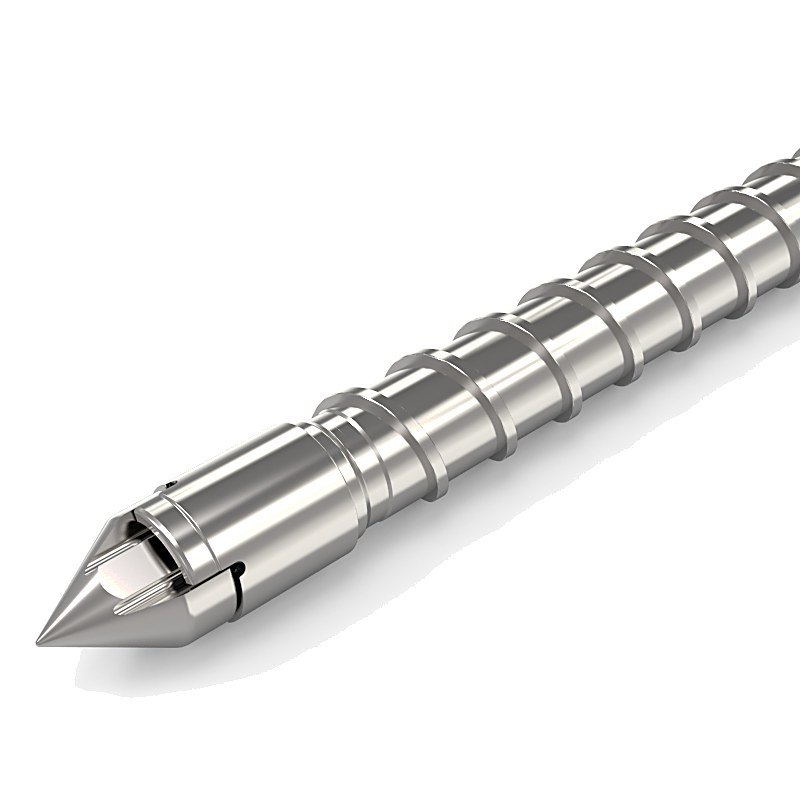
Three-zone GP screw for PE, PP, PS and ABS with polished flight profile.
View Details →Send your machine model, drawing or worn sample — we reply with a matching proposal and quotation within one business day.