Screw and barrel sets for XPS (extruded polystyrene) foam board lines — built for the high temperature, high head pressure and foaming-agent environment that destroys ordinary barrels.
XPS foam board is produced by extruding polystyrene compound with a foaming agent under high temperature and high head pressure, then cooling and calibrating the melt into board. The plasticizing unit on an XPS line works far harder than on ordinary extrusion: sustained high pressure before the die, foaming agent injected near the end of the screw, and long continuous runs at full load.
Under these conditions ordinary nitrided barrels lose clearance steadily. Melt leaks back, head pressure drops, and board density and cell structure drift out of specification. Our XPS sets pair a bimetallic-lined barrel with a screw built for your foaming agent — CO2, butane, HFC or DMS systems — so melt pressure stays stable for the whole service life of the set.
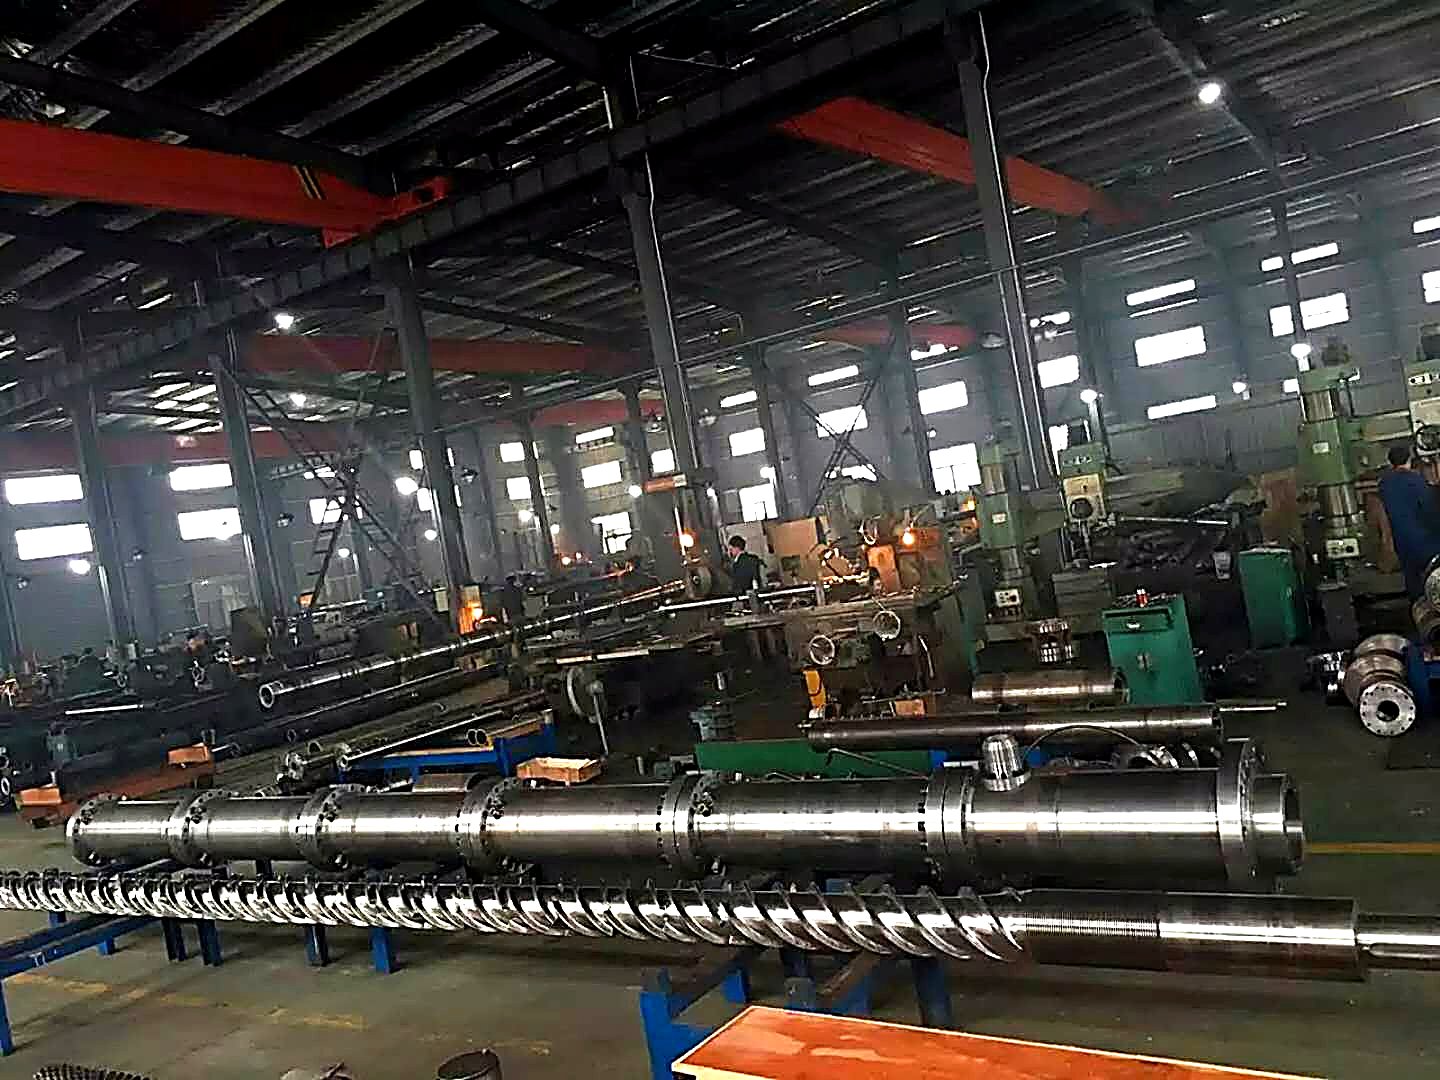
Single screw designed for stable PS melting with foaming agent injection near the screw tip.
Bimetallic-lined barrel matched to the screw, with grooved feed option for high output.
Machined port body for CO2, butane or HFC injection with leak-tight fittings.
Downstream mixing elements for uniform cell structure across the board.
Connection pieces between barrel and die, machined to your line layout.
Worn XPS barrels re-bored and re-lined; screws re-flighted and re-coated.
Screw, barrel and drive-matched components supplied as one package.
Seals, heaters, thermocouples and wear parts for line maintenance.
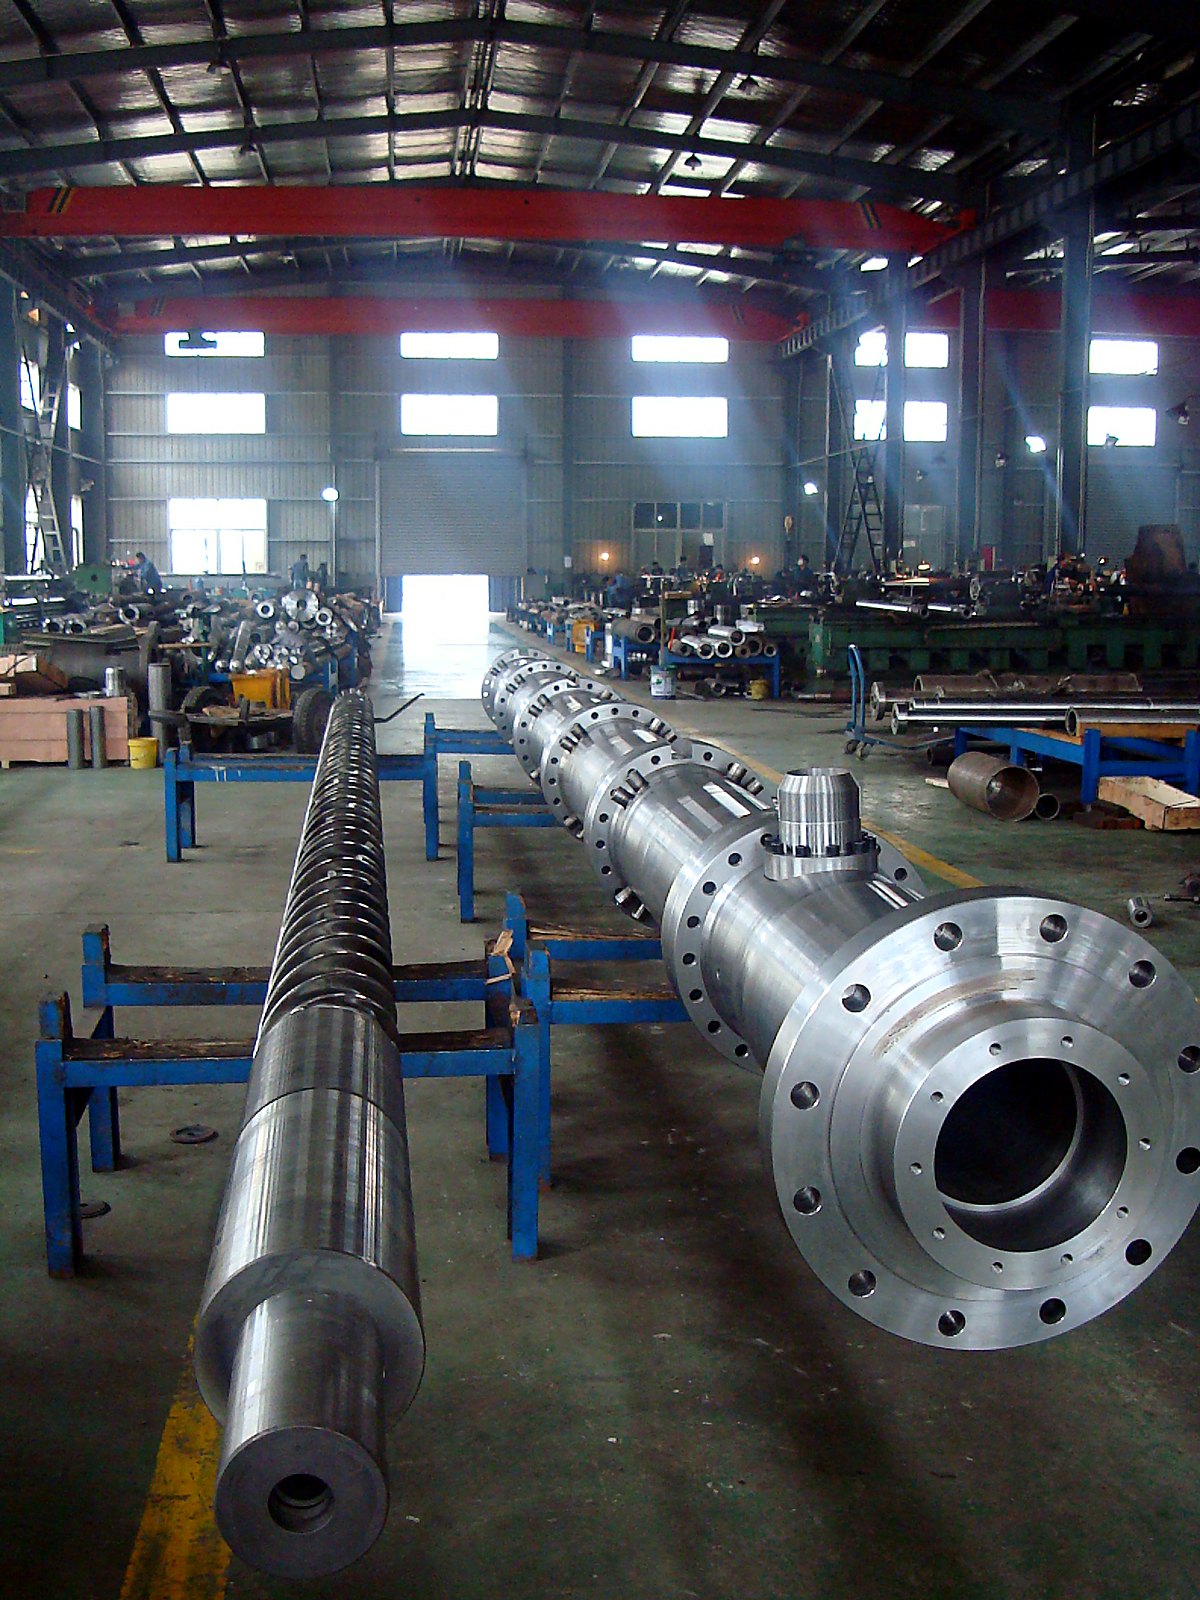
Complete set for XPS foamed board production lines.
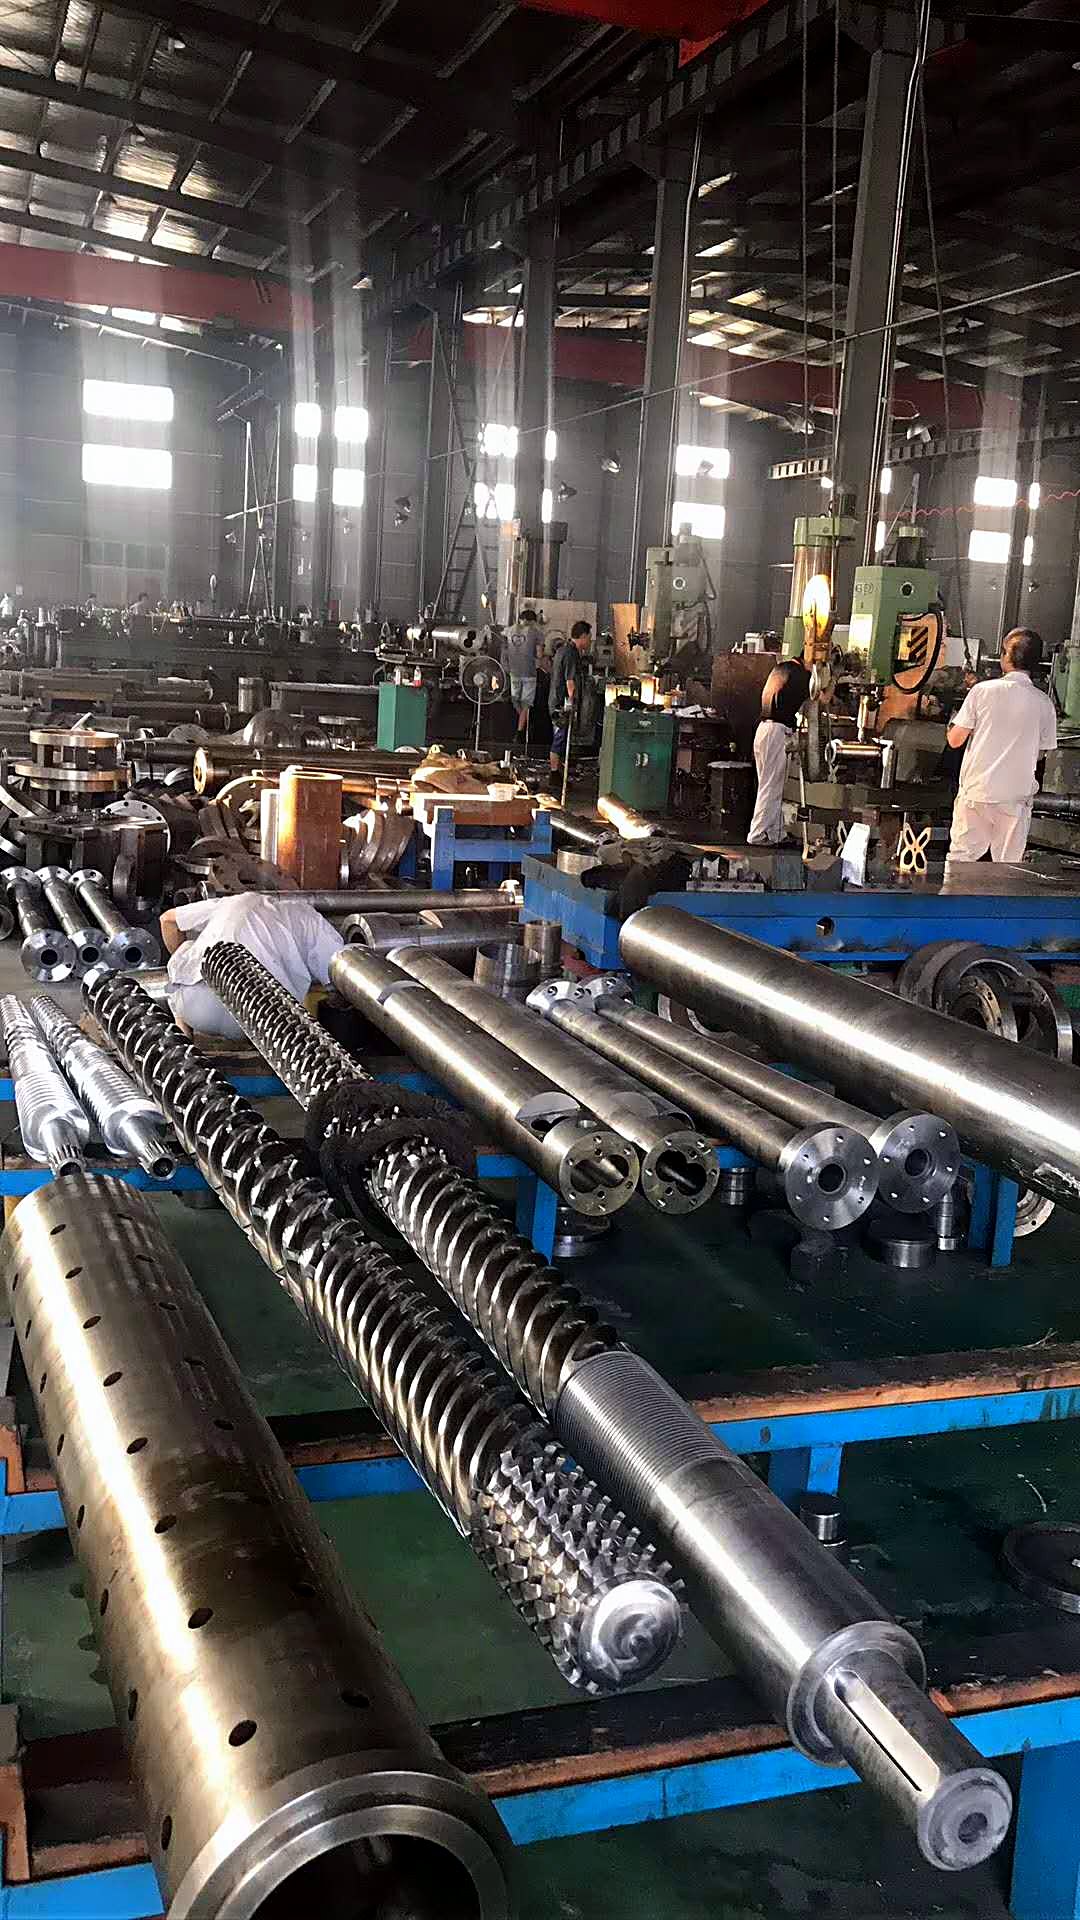
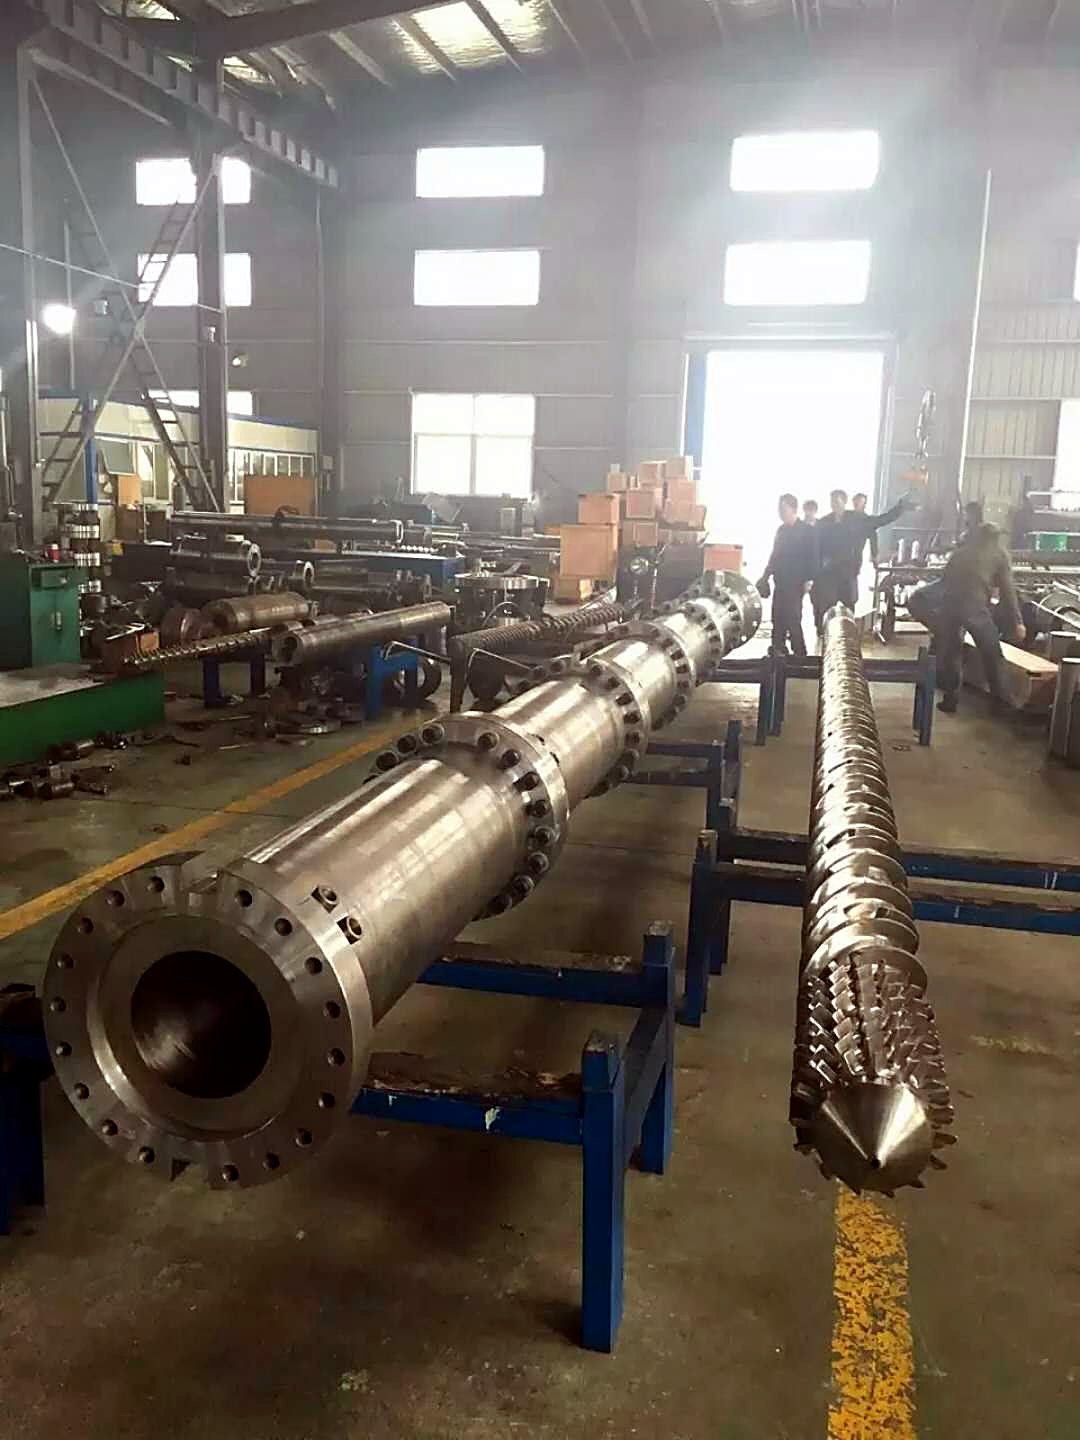
Barrel for XPS foaming extruder with temperature-control design.
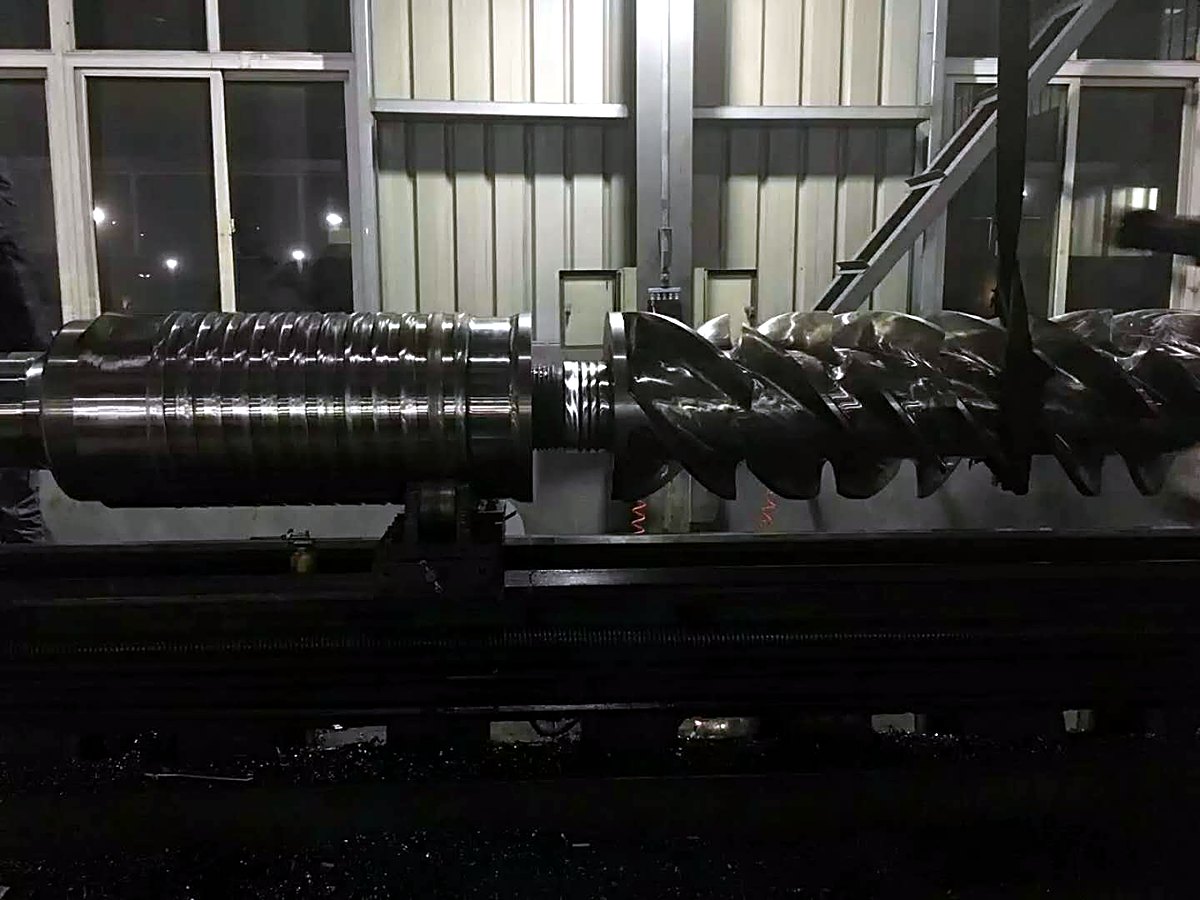
Big-format XPS screw sets, max machining diameter Ø300 mm in-house.
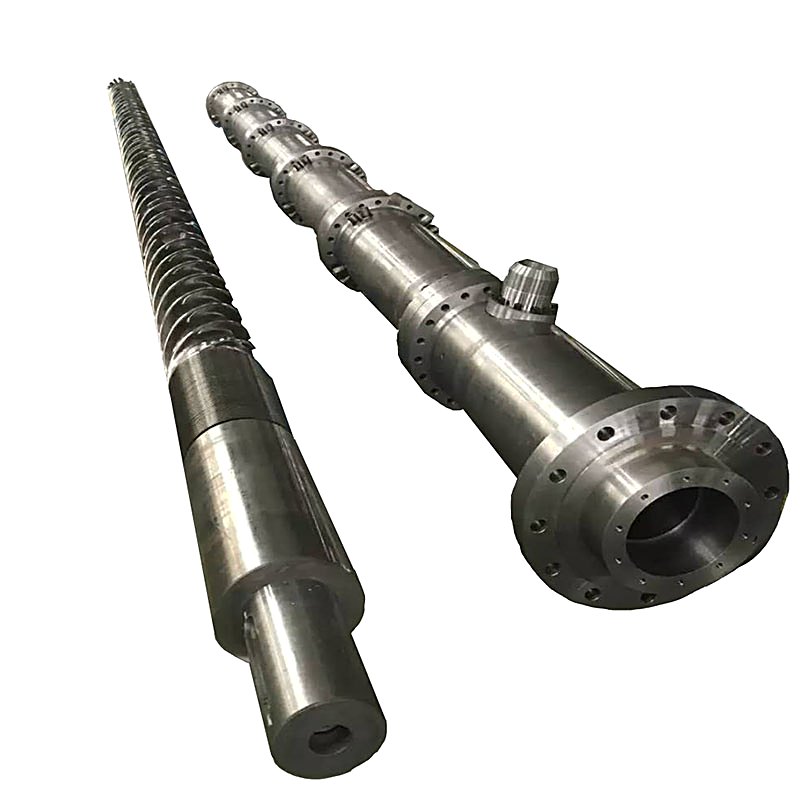
XPS foamed screw barrel configured for CO₂ and butane physical blowing agents.
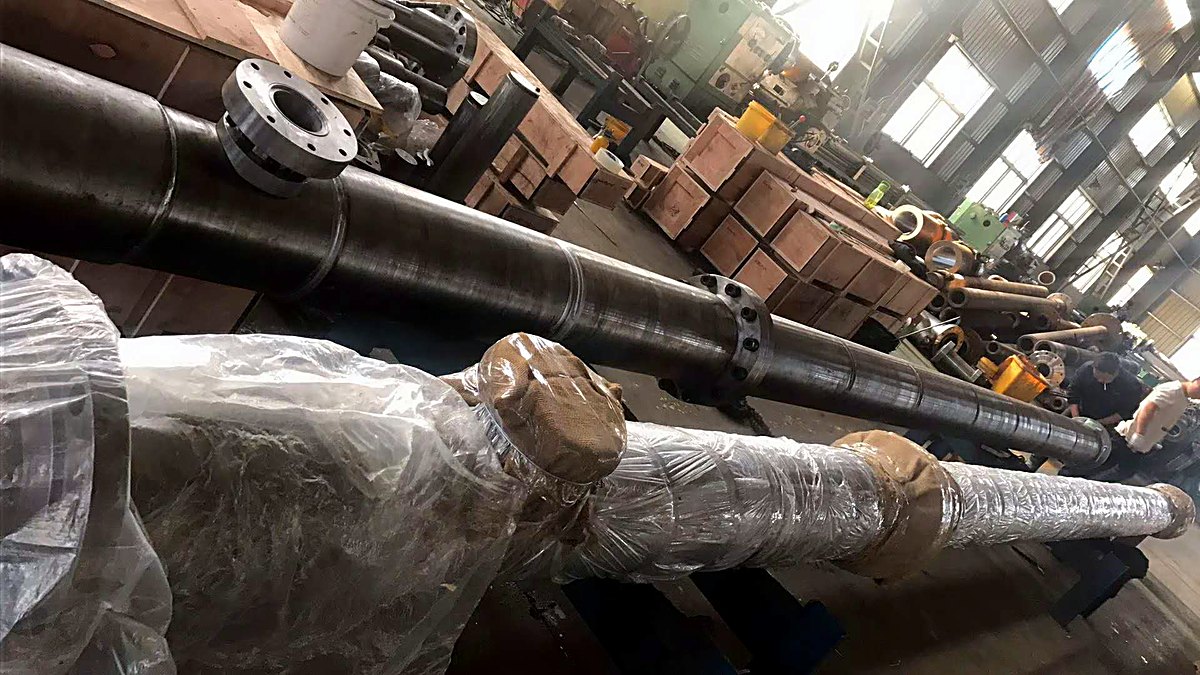
High-output XPS screw barrel sized for 1200 mm board and heavy-duty lines.
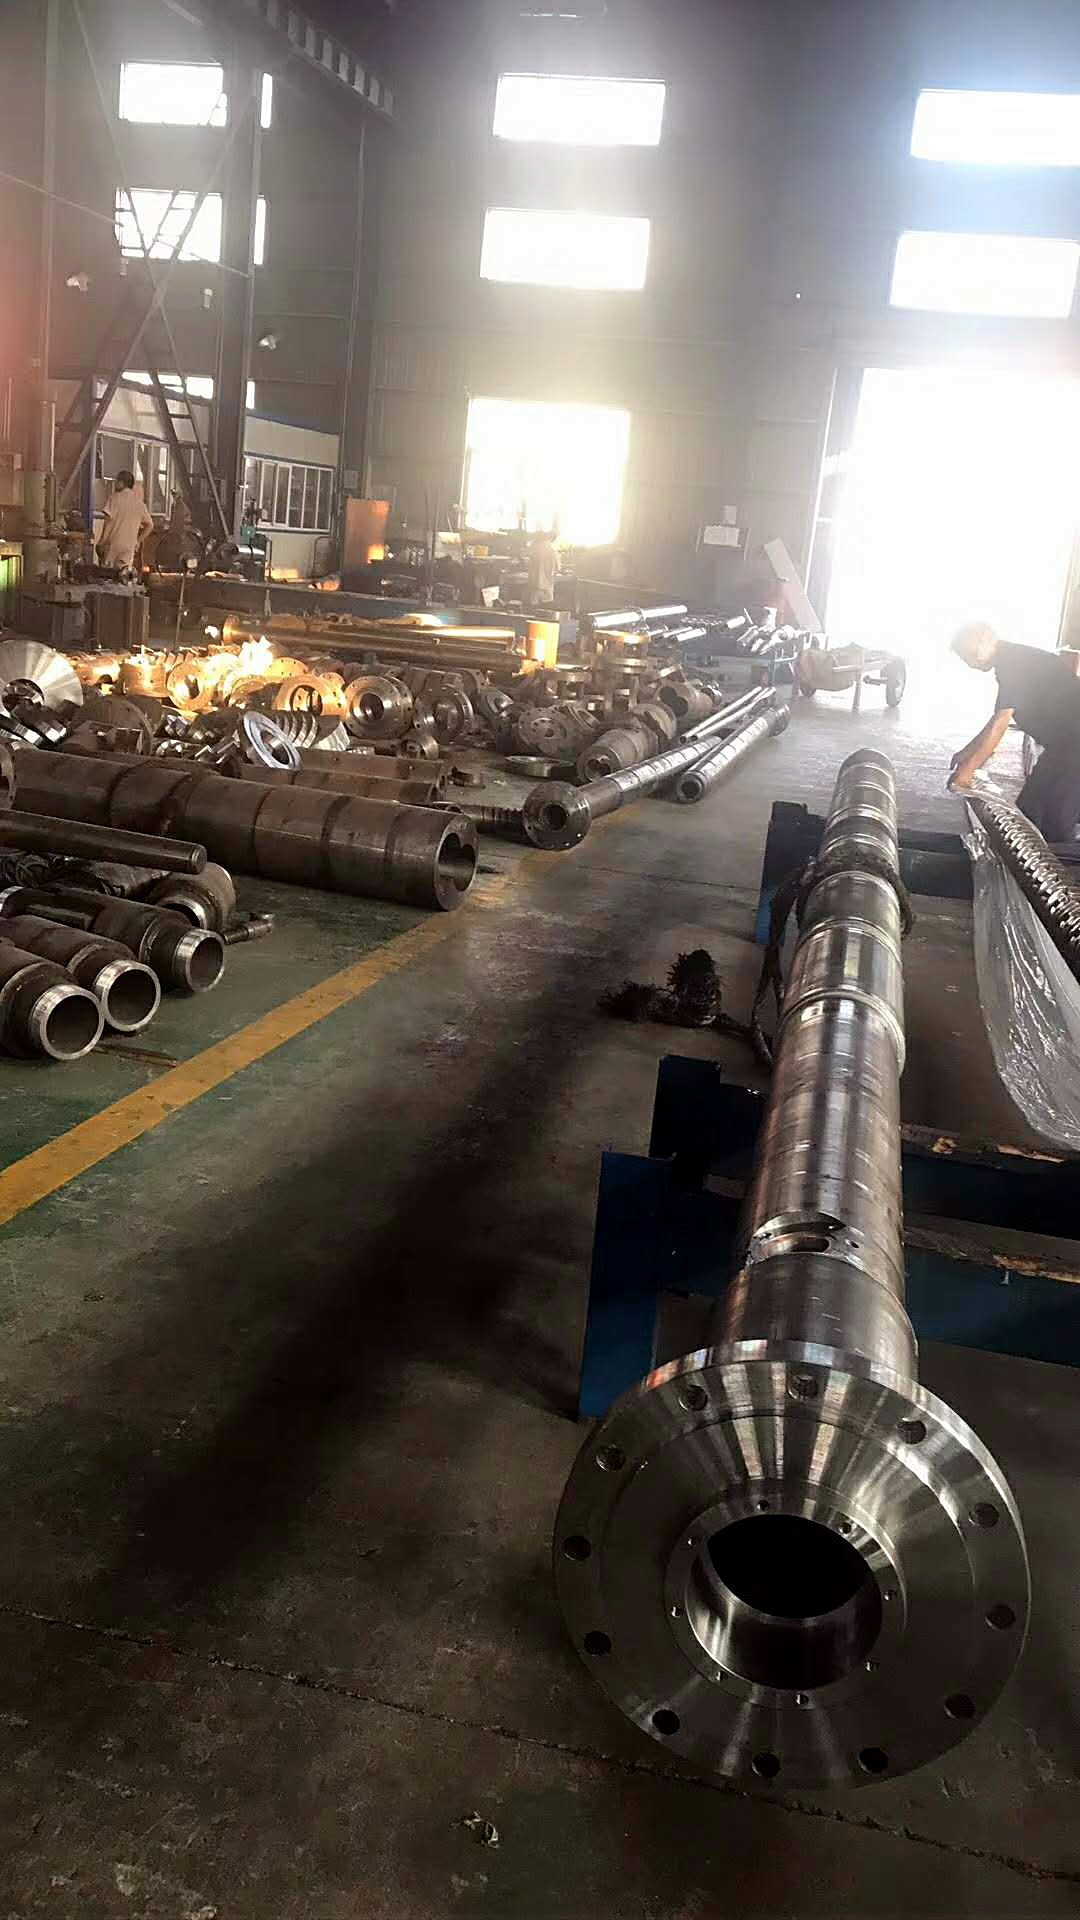
XPS screw barrel tuned for B1-class flame-retardant XPS compound duty.
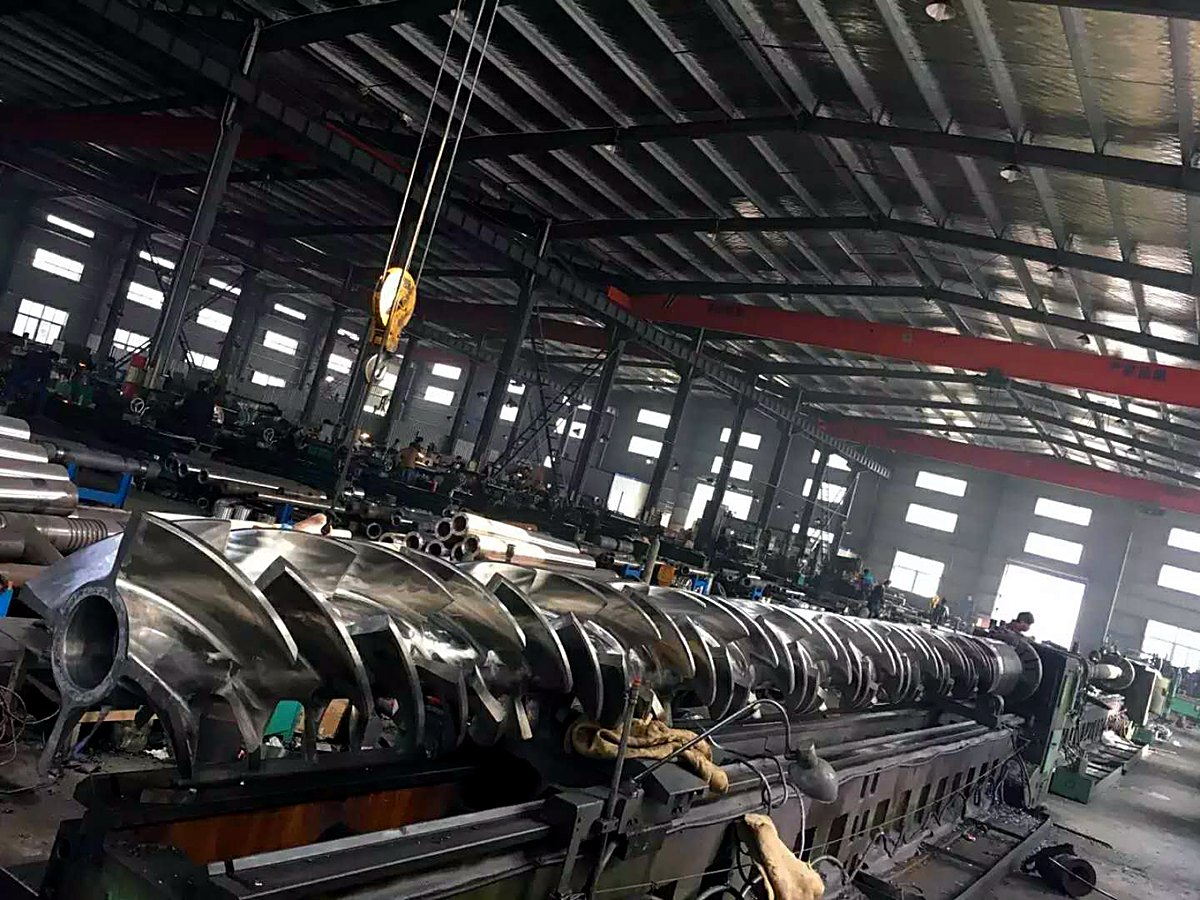
XPS screw barrel for graphite-enhanced black board with even dispersion duty.
New models are added regularly — or send your drawing or worn sample for a custom build.
Standard ranges shown below. Non-standard sizes and custom geometry are built to your drawing or sample.
| Item | Specification |
|---|---|
| Application | XPS foam board / insulation board production lines |
| Screw Diameter | Per your line — commonly Ø65–Ø150 mm |
| Foaming Agent | CO2, butane, HFC or DMS systems |
| Barrel Construction | Bimetallic-lined, corrosion-resistant alloy layer |
| Lining Hardness | HRC 55–72, metallurgically cast layer |
| Supply Basis | Built to line model, drawing or worn sample |
Material and treatment are selected by the resin you process, filler content and expected service life.
Nickel-based alloy layer resists both mechanical wear and foaming-agent corrosion.
38CrMoAlA gas-nitrided screws for lines running clean, non-corrosive formulas.
We review your formula, output rate and running hours before selecting materials.
Machined to your heating zones and sensor positions for stable XPS melting.
Barrel and flange design rated for the high head pressure of XPS extrusion.
Spectral analysis and certificates for every batch of bar stock.
Common problems we help injection and extrusion plants solve — and how a matched screw barrel fixes them.
A worn bore lets melt leak back, so foaming becomes uneven across the board.
Stable bore tolerance keeps melt pressure — and cell structure — uniform.Abrasion from the compound and corrosion from the agent cut output steadily.
Bimetallic lining resists both attack modes for a longer service life.Some foaming agents and decomposition residues pit nitrided surfaces.
Corrosion-resistant alloy layer formulated for foaming duty.A failed barrel in peak season costs board output exactly when demand is highest.
Long-life sets and rebuild service keep maintenance in planned windows.Generic barrels leak at flanges and injection ports.
Machined to your line model — flanges, ports and heater seats line up.Suppliers who never ran an XPS line cannot advise on material selection.
18 years supplying XPS line components, with formula-based material advice.You send the line model, output target and foaming agent type.
We match screw coating and barrel lining to your formula and duty.
Screw flights and barrel bore machined with verified tolerances.
Nitriding or bimetallic lining, with hardness verified on coupons.
Hardness, bore geometry and runout checked and recorded.
Rust protection, wooden case, sea / air / express shipment.
Insulation boards for construction, from standard to high-density grades.
Wall, roof and under-slab insulation board production.
XPS boxes and sheets for temperature-controlled packaging.
Insulation boards for greenhouses and livestock buildings.
XPS panels routed for underfloor heating systems.
XPS combined with facings for structural insulated panels.
Boards cut and profiled for special construction details.
Components supplied to XPS line manufacturers as OEM parts.
Replacing worn units on existing XPS lines to restore output.
“Our old barrels lasted eight months on butane foam. The new bimetallic set is past a year with stable board density.”
Production ManagerXPS board producer, Middle East“They asked for our formula and output rate before quoting — nobody else did that. The set fitted perfectly.”
Plant EngineerInsulation materials manufacturer“Rebuilt our worn screw instead of selling us a new one. That saved the season's output.”
Maintenance SupervisorConstruction materials plantYes. Send the line brand and model, screw diameter and a photo of the worn set. We reverse-engineer the geometry and confirm dimensions with you before machining starts.
CO2, butane, HFC and DMS systems. We select the barrel lining and screw coating based on the agent and the abrasiveness of your formula.
Often yes — we re-bore and re-line worn barrels and re-flight screws. Send photos and measurements and we will assess whether a rebuild is economical for your case.
Usually growing clearance between screw and barrel. Melt leaks back, head pressure drops and foaming becomes uneven. A matched wear-resistant set restores stability.
It depends on formula and running hours. With bimetallic lining and correct material selection, service life is typically several times longer than ordinary nitrided sets on the same line.
Typically 25–40 days after drawing confirmation, depending on diameter and lining. Rush service is available for line-down emergencies.
Send the drawing, machine model or worn sample — we confirm the geometry and quote within one working day.
Tell us the machine model, screw diameter and material you process — we will reply with a matched solution and quotation.
Or write directly to info@xiwangindustry.com · WhatsApp +86-13503734287
Yes. XPS sets are built for the combination of abrasive and corrosive duty these agents create, with alloys selected for both properties rather than only for wear.
Foaming duty runs at high pressure with a blowing agent that attacks the bore surface while the polymer itself carries abrasive additives. A general-purpose extruder barrel built to ordinary specification will not survive it, which is why these lines need a dedicated construction.
Yes — first-stage and second-stage screws and barrels can be supplied together so temperatures and pressures across the line stay balanced. Send both stage specifications and we quote them as one package.
Tell us your machine model, drawing or worn sample — we reply with a matching proposal and quotation within one business day.