Planetary screw barrels with multiple planet rolls around a central screw, delivering intensive dispersive mixing and high output for PVC compounding and calender feed.
A planetary screw barrel has a central (sun) screw surrounded by several smaller planet screws that rotate around it inside the barrel bore. Material passing through the spiral groove moves from the large space around the central screw into the narrow gaps around the planet rolls and back again.
That repeated expansion and compression, combined with the planet rolls' own rotation, subjects material to strong deformation and stretching. The effect is intensive dispersive mixing, while residence time stays much shorter than in a single screw — so mixing quality and output both improve.
These characteristics make the planetary design a strong fit for PVC compounding and calender feed preparation, where thorough gelation and dispersion must be achieved without thermal degradation.
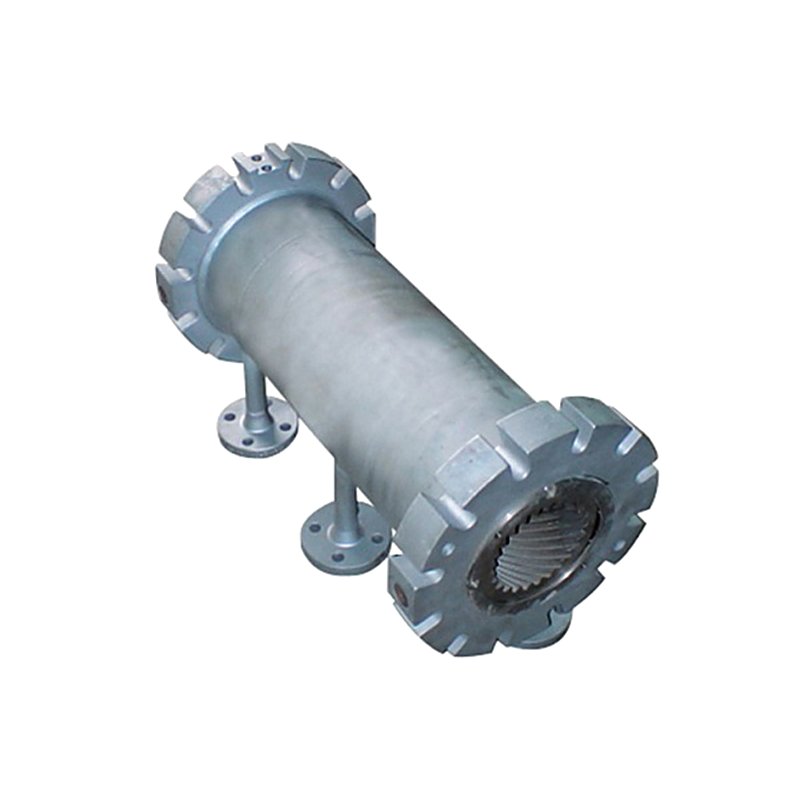
Central screw with surrounding planet rolls for PVC compounding.
Several planetary zones in series for progressive mixing intensity.
Planetary section preparing homogenised compound for the calender.
Individual planet rolls supplied as replacement spares.
Central sun screw supplied individually or with the set.
Planetary barrel section with matching internal geometry.
Built to your drawing or reverse-engineered from the worn unit.
Segment and roller layouts tuned to your dispersion target.
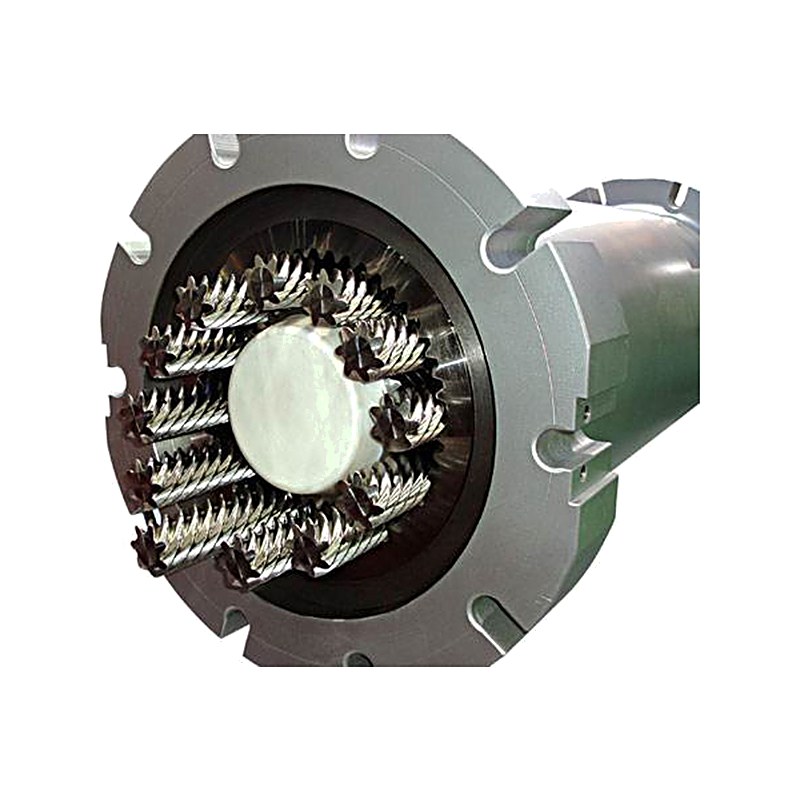
For planetary roller extruders in rigid PVC compounding and calendering.
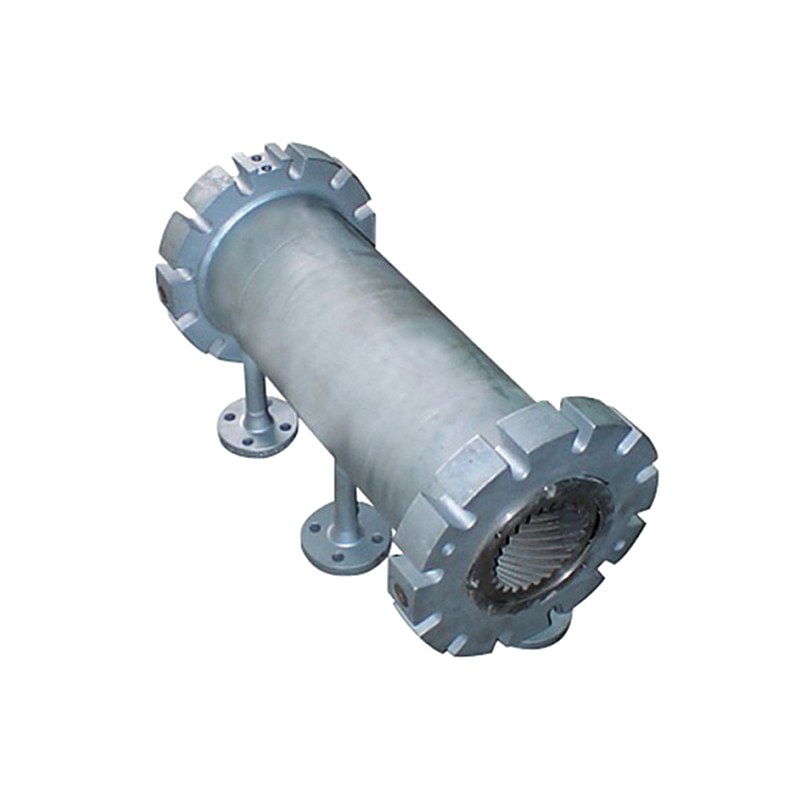
Central spindle with helical flights matched to the roller set.
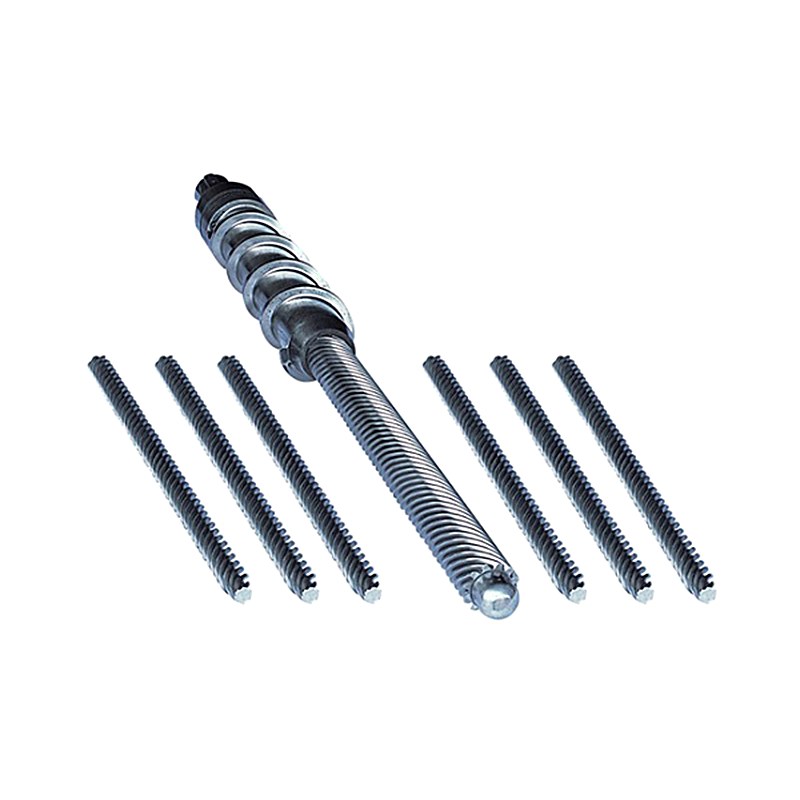
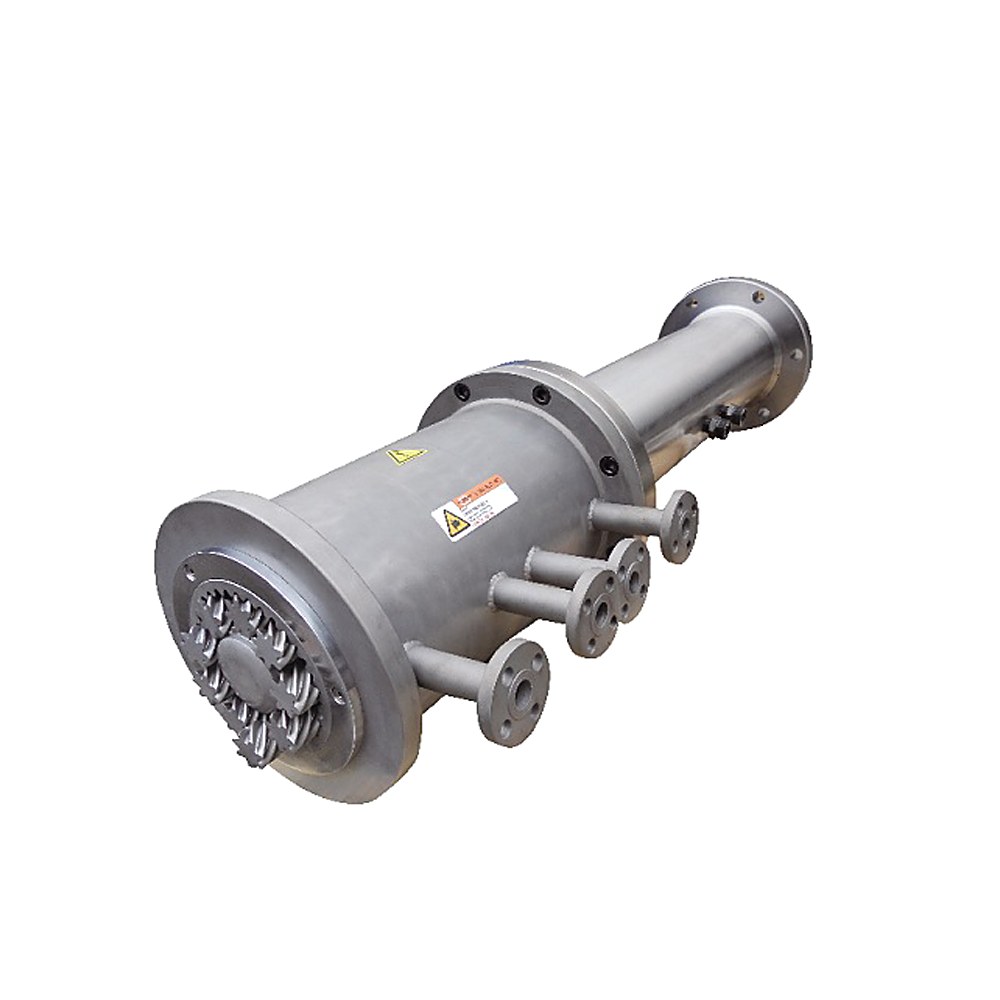
Hardened planetary roller sets, supplied as matched sets.
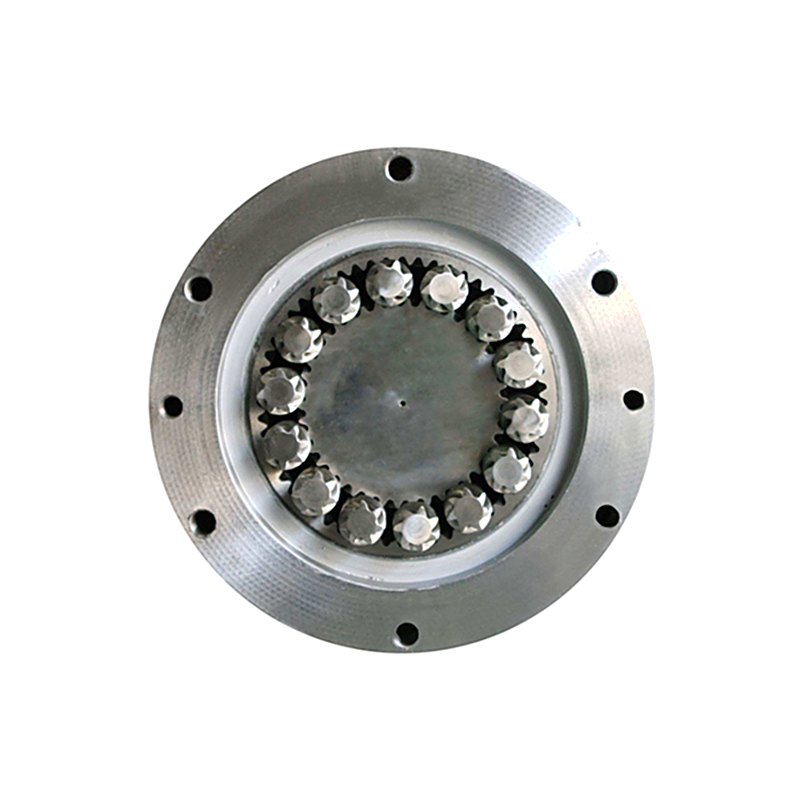
Planetary screw barrel for rigid PVC calendering feed and large-area sheet lines.
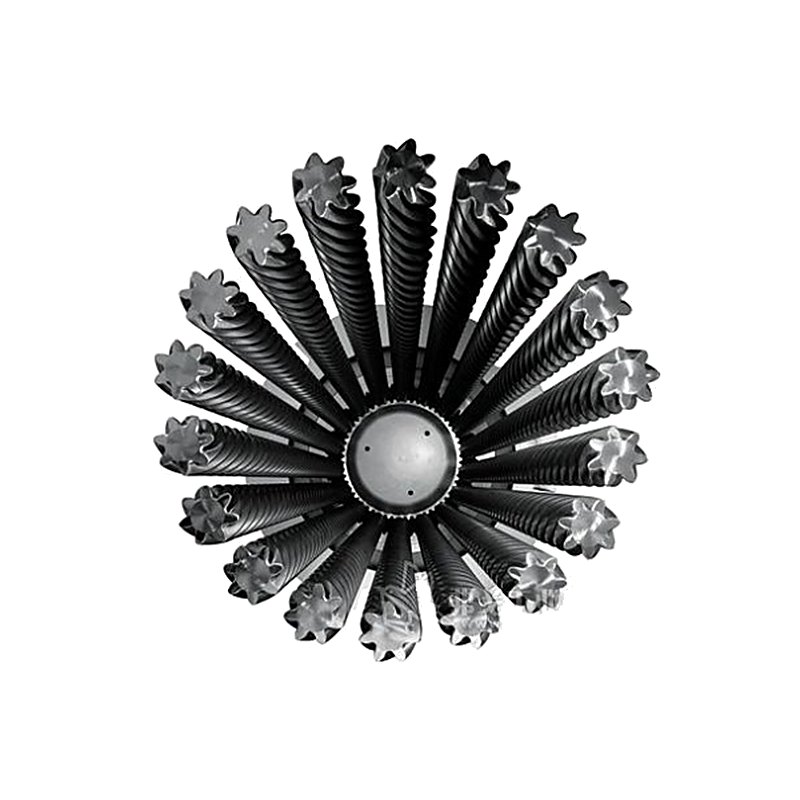
Planetary screw barrel for rigid PVC pipe, fitting and profile feed applications.
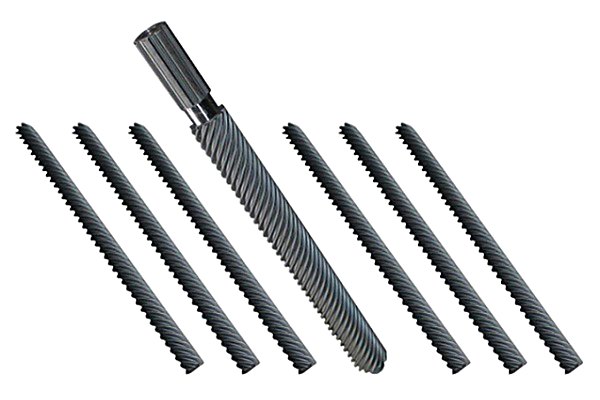
Replacement planetary roller spindles, matched sets for 7 / 9 / 12 spindle sections.
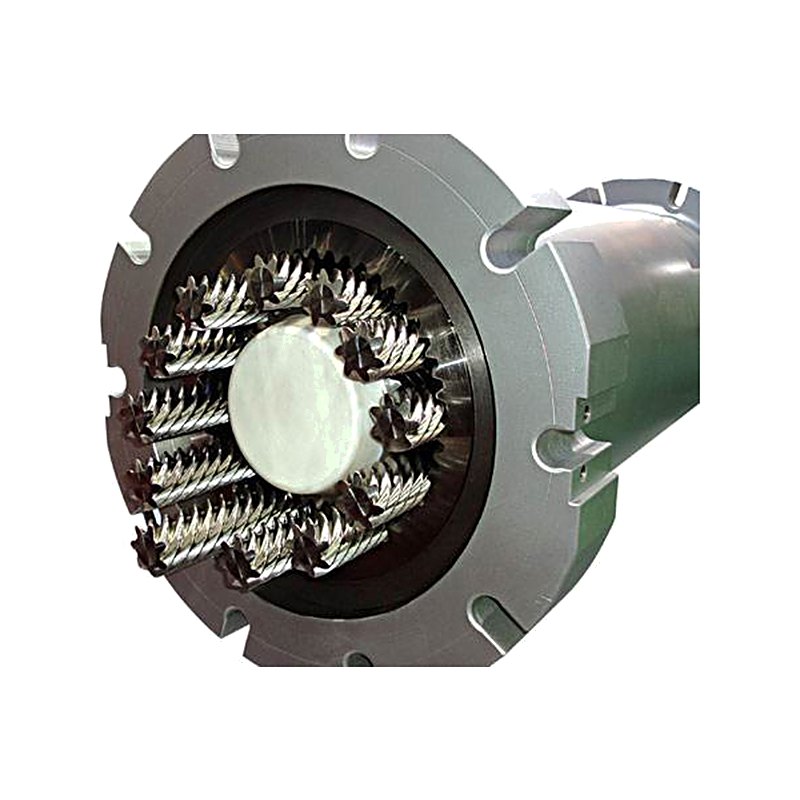
Planetary screw barrel for plasticised PVC cable compound preparation.
New models are added regularly — or send your drawing or worn sample for a custom build.
Standard ranges shown below. Non-standard sizes and custom geometry are built to your drawing or sample.
| Item | Specification |
|---|---|
| Configuration | Central screw with surrounding planet rolls (planetary gear design) |
| Working Principle | Repeated expansion / compression of material flow for intensive dispersive mixing |
| Key Advantage | Better mixing and higher output with much shorter residence time than single screw |
| Typical Application | PVC compounding, calender feed preparation |
| Base Material | 38CrMoAlA, 42CrMo, high-alloy tool steel, stainless steel |
| Nitriding Depth | 0.4 – 0.7 mm, surface hardness HV 900–1100 |
| Surface Treatment | Nitriding, bimetallic lining or hardfacing depending on formulation |
| Machining Tolerance | ±0.02 mm on critical fits |
| Spare Parts | Planet rolls, central screw and barrel sections available individually |
| Lead Time | Confirmed with quotation depending on configuration |
Material and treatment are selected by the resin you process, filler content and expected service life.
Standard for PVC compounding with moderate filler loading.
For planet rolls and screws running abrasive filled PVC formulations.
For high filler content or recycled PVC where abrasion dominates.
For corrosive formulations and hygiene-sensitive applications.
Additional wear protection on planet roll and screw surfaces.
Nitrided, ground segments built for roller engagement accuracy.
Common problems we help injection and extrusion plants solve — and how a matched screw barrel fixes them.
PVC compound reaches the calender not fully gelled, showing gels and fisheyes.
Intensive dispersive mixing in the planetary zone completes gelation.Additives and pigment are not distributed uniformly through the compound.
Repeated deformation in the planetary gaps improves dispersion markedly.Long residence in a single screw overheats heat-sensitive PVC.
Short residence time in the planetary unit reduces thermal exposure.Mixing quality limits how fast the line can run.
Planetary design raises output while improving mixing.Rolls lose profile and mixing intensity drops over time.
Replacement rolls restore mixing performance without replacing the whole unit.Worn planetary segments lose kneading and dispersion efficiency.
Replaced segment sets restore original dispersion quality.Formulation, filler level and downstream process define zone count and geometry.
Central screw, planet roll count and barrel section geometry specified.
Precision boring and gear-profile machining with treatment allowance.
Nitriding, bimetallic lining or tool-steel hardening per selection.
Grinding of rolls, screw and bore to final tolerance.
Rolls fitted, clearances and rotation verified, then packed.
Rigid and flexible PVC compound production.
Homogenised compound feed for calendering lines.
Calendered film and sheet production.
Compounds with calcium carbonate and other fillers.
Dispersion-intensive colour preparation.
Re-compounding of PVC recyclate.
“Gelation is much more complete since the planetary section was installed. Fisheye complaints dropped.”
Quality ManagerCalendered film producer, Europe“We get better dispersion at higher output than the single screw we ran before.”
Process EngineerPVC compounder, Asia“Replacement planet rolls arrived matching the original geometry, so the changeover was quick.”
Maintenance LeadSheet producer, South AmericaMaterial repeatedly moves between the wide space around the central screw and the narrow gaps around the planet rolls, undergoing strong deformation each time. Residence time is shorter than in a single screw while mixing is far more intensive.
Yes. We supply planet rolls, the central screw and barrel sections individually as spare parts, matched to your existing unit.
Commonly nitrided alloy steel or high-alloy tool steel, with bimetallic or hardfaced options for abrasive, highly filled formulations.
Yes — central screw, planet rolls and barrel section as a matched assembly, built to your drawing or from the worn unit.
Machine or unit model, formulation with filler type and level, downstream process, and a drawing or the worn parts if available.
It depends on configuration, size and treatment. The schedule is confirmed together with the quotation.
Send the drawing, machine model or worn sample — we confirm the geometry and quote within one working day.
Tell us the machine model, screw diameter and material you process — we will reply with a matched solution and quotation.
Or write directly to info@xiwangindustry.com · WhatsApp +86-13503734287
Yes. Central screw, planetary spindles and the barrel itself can be rebuilt or supplied new. Because the parts must work as a matched set, we prefer to quote the whole assembly together so clearances stay consistent.
Planetary gear sections see rolling contact plus abrasion. We nitrided or use a wear-resistant alloy depending on filler loading, and we will discuss the duty before recommending, because planetary assemblies are expensive to get wrong.
Not necessarily. Send a sample set or clear dimensions and we reverse-engineer the tooth form and pitch, then confirm it with a drawing before machining. This is standard practice for older machines whose builders no longer support them.
Tell us your machine model, drawing or worn sample — we reply with a matching proposal and quotation within one business day.