Complete matched set for 90–450 t injection moulding machines, nitrided or bimetallic. Machined in our own Henan workshop — to your drawing, or reverse-engineered from your worn parts.
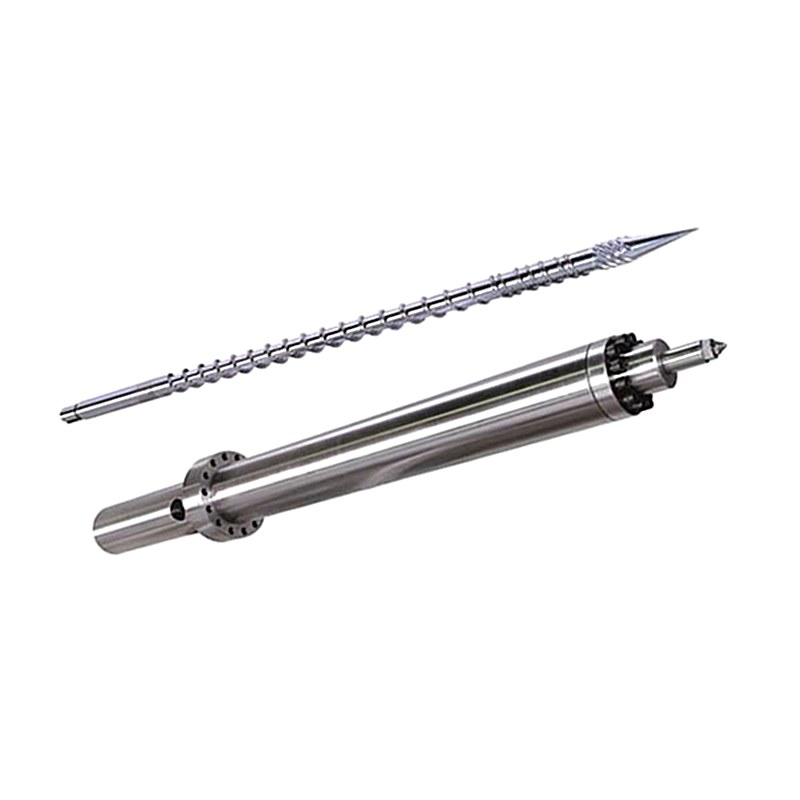
A matched screw and barrel set is the fastest way to restore shot weight consistency on an injection machine. We machine both parts from one order, so the clearance between flight land and barrel bore is set by us — not left to chance.
Send us the machine brand, tonnage and screw diameter, or simply the worn parts. We reverse-engineer the geometry, confirm the drawing with you, then machine, nitride and finish the set in our own workshop in Henan.
Quote within one business day. We reply with a matching proposal, delivery date and price — no generic catalogue PDF.
Standard range shown. Every dimension below can be changed to your machine, resin and output — custom manufacturing is our daily business.
| Screw diameter | Ø20–150 mm |
|---|---|
| L/D ratio | 16–26 (custom on request) |
| Base material | 38CrMoAlA / 42CrMo / bimetallic |
| Nitrided hardness | HV 900–1020, depth 0.45–0.7 mm |
| Barrel bore finish | Honed / deep-hole bored, Ra 0.4 |
| Fit clearance | 0.10–0.20 mm, matched per set |
| Lead time | 25–35 days after drawing approval |
The honest answer depends on your resin, not on price. Here is how we advise customers.
| Gas Nitrided (38CrMoAlA) | Bimetallic Alloy Lining | |
|---|---|---|
| Best for | Unfilled PE, PP, PS, ABS, virgin PVC | Glass-filled, mineral-filled, recycled, corrosive |
| Surface hardness | HV 900–1020, depth 0.45–0.7 mm | Alloy layer 2–5 mm, metallurgically bonded |
| Typical service life | Baseline | 3–5× baseline on abrasive resin |
| Cost | Lower | Higher, recovered through fewer stoppages |
| Certification | MTC with heat number | MTC + hardness records, third-party on request |
Yes. We build to Engel, Arburg, Haitian, Toshiba, JSW, Demag, KraussMaffei, Battenfeld and most Chinese brands. Give us the brand and tonnage and we check our records first.
Nitrided suits unfilled resins (PE, PP, PS, ABS). Switch to bimetallic if you run glass fibre, mineral fillers, flame retardant or PVC, or if you are replacing a set that wore out in under two years.
Machine model, screw diameter, L/D and resin. A photo of the nameplate plus three dimensions is usually enough; a drawing or the worn sample is better.
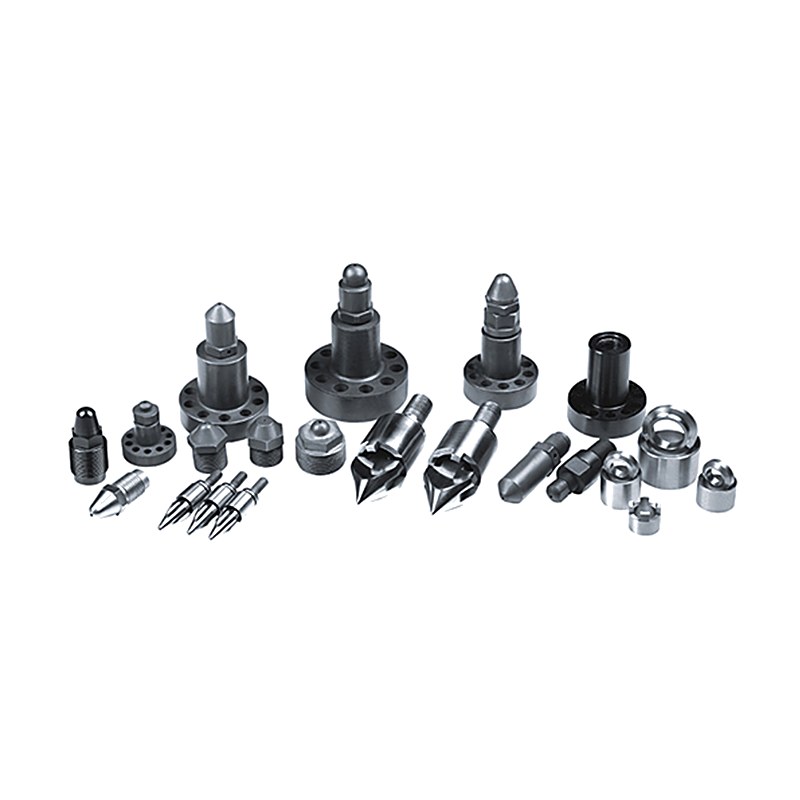
High-compression PET screw with barrier tips, low acetaldehyde generation for bottle-grade preforms.
View Details →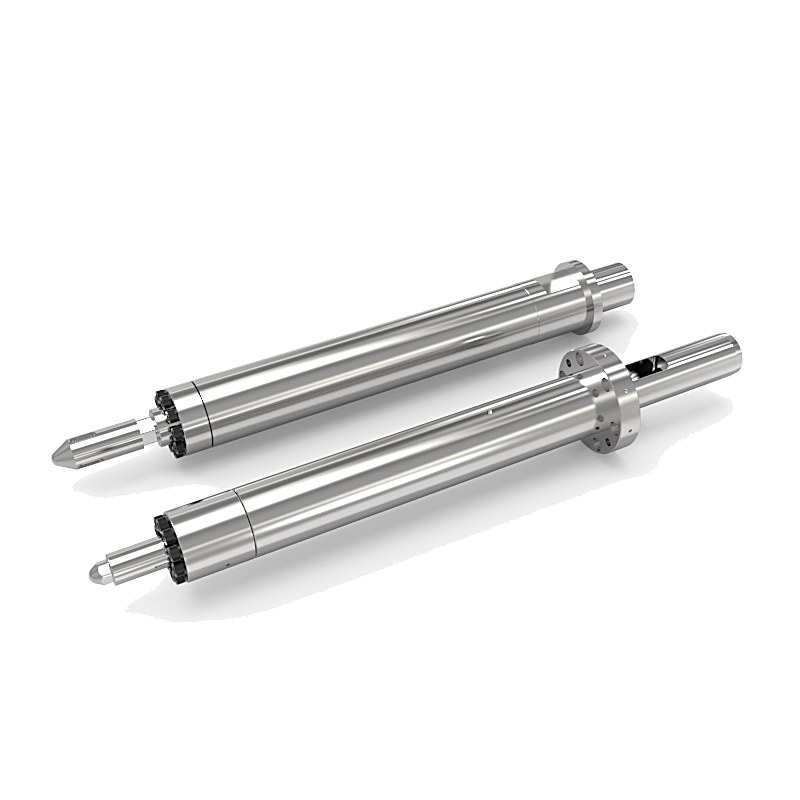
Centrifugally cast 2–5 mm alloy lining for glass-filled and corrosive resins.
View Details →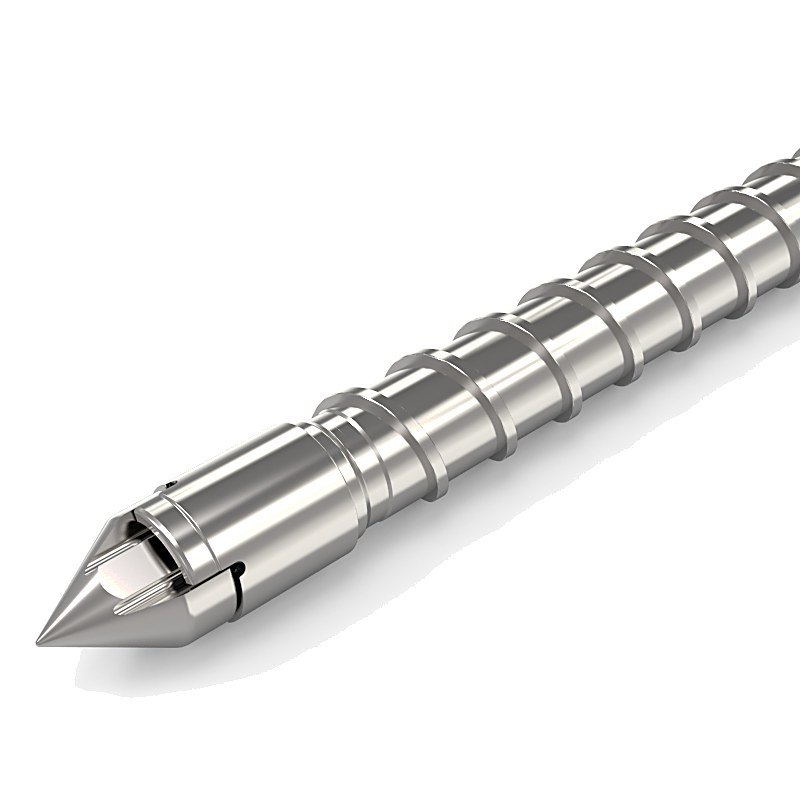
Three-zone GP screw for PE, PP, PS and ABS with polished flight profile.
View Details →Send your machine model, drawing or worn sample — we reply with a matching proposal and quotation within one business day.