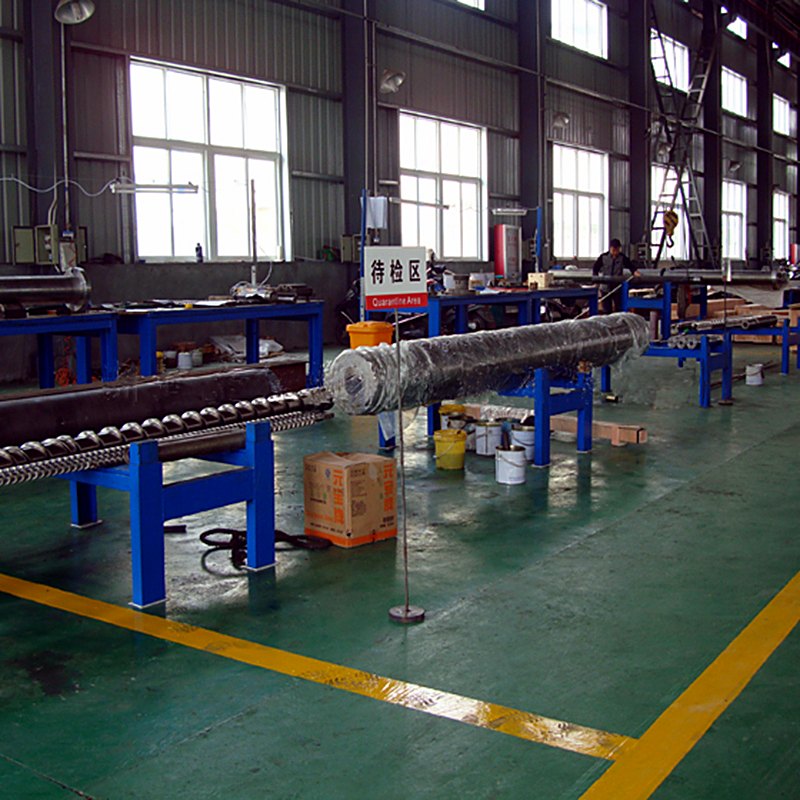
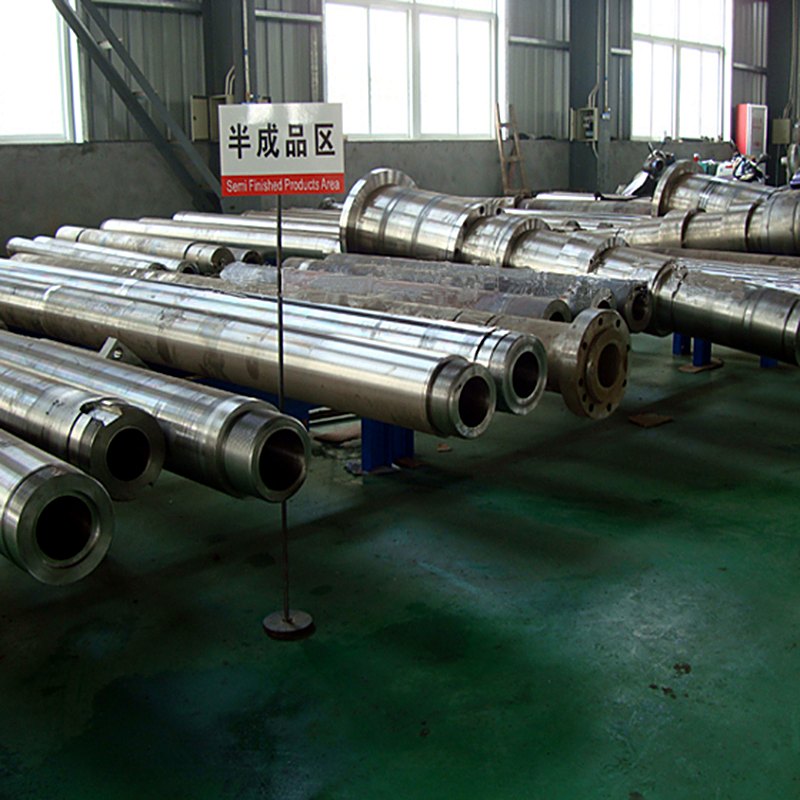
14,000+ m² of manufacturing space in Henan — casting, machining, heat treatment and inspection under one roof.
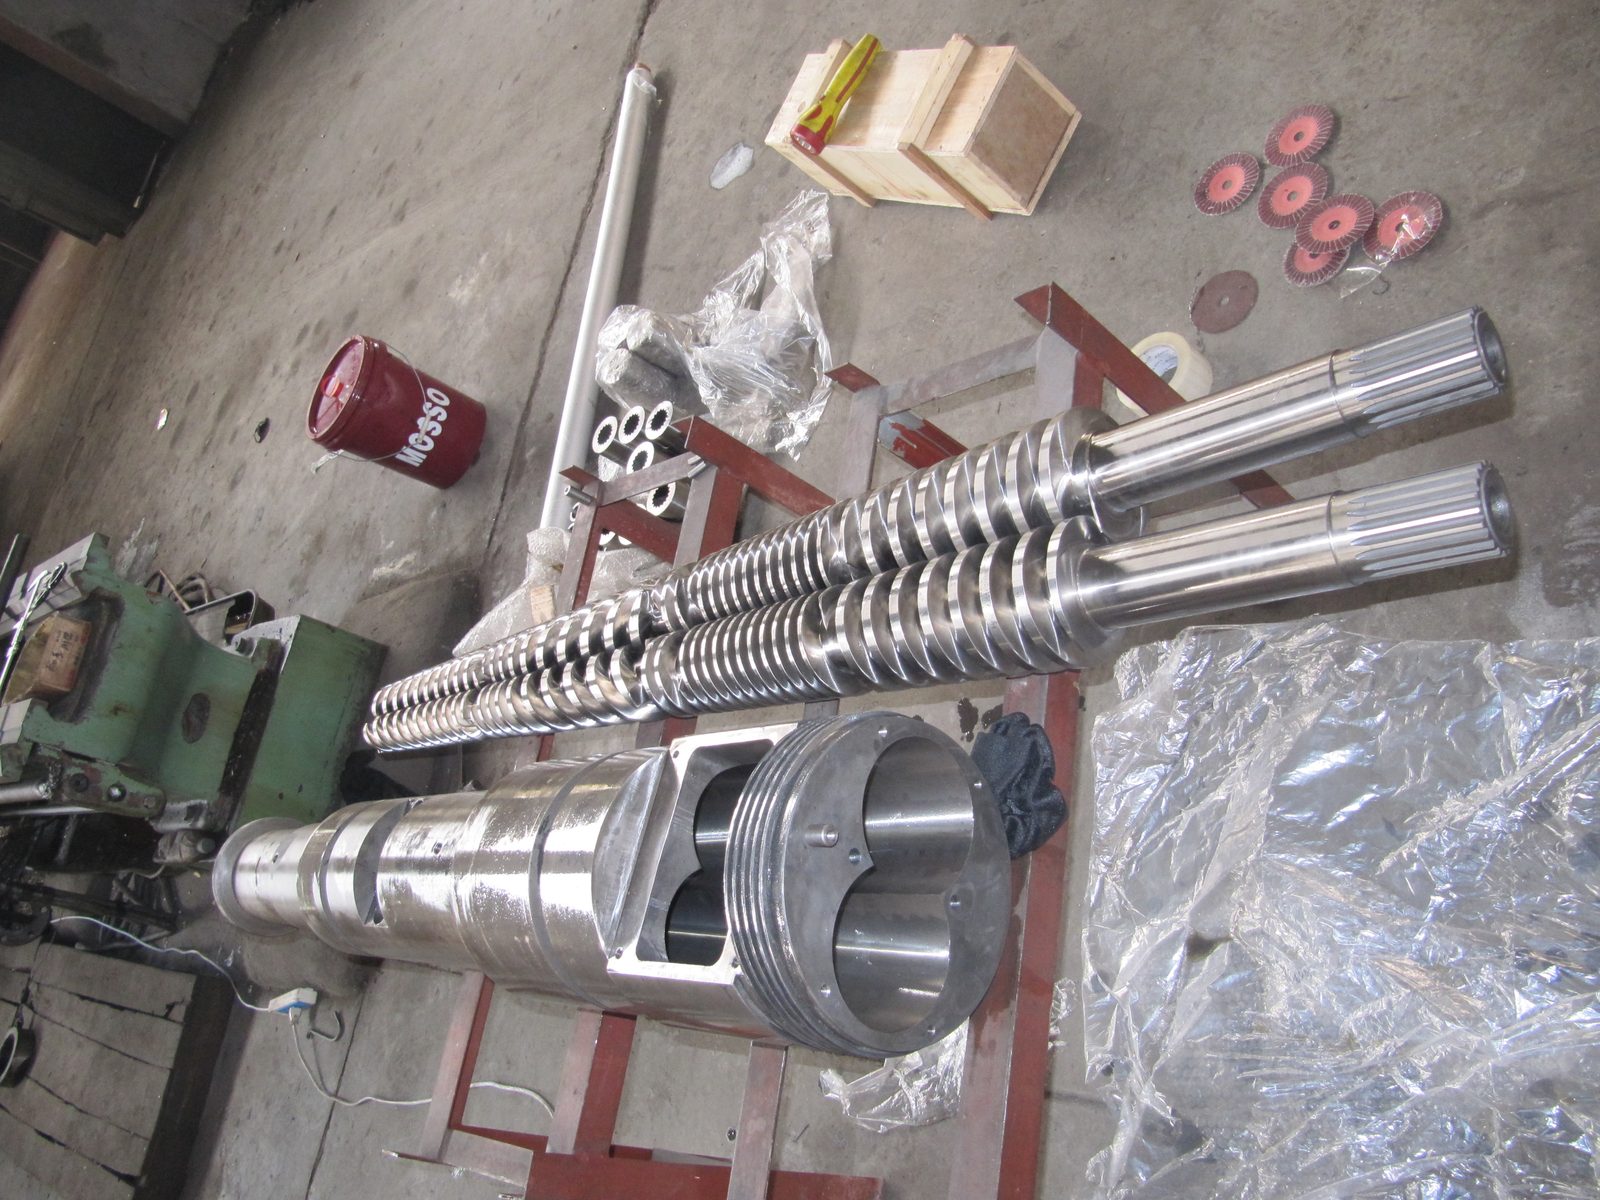
Every step that determines the life of a screw barrel happens in-house: centrifugal bimetallic casting, gas nitriding, deep-hole boring, thread milling, grinding and final inspection. Keeping the full process under our own roof is how we hold tolerances and control lead times — nothing critical is outsourced.
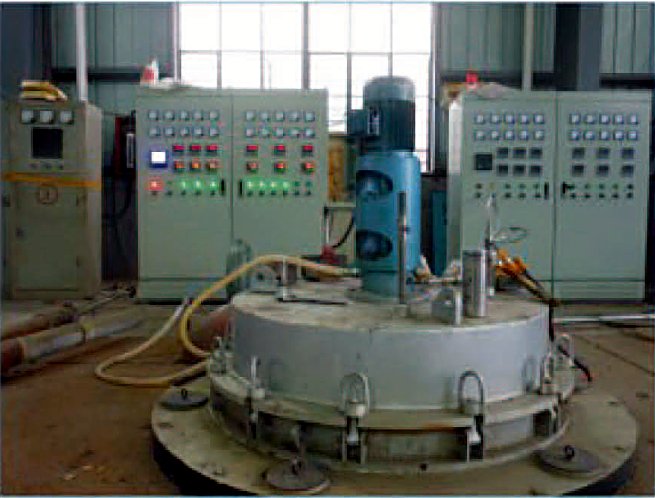
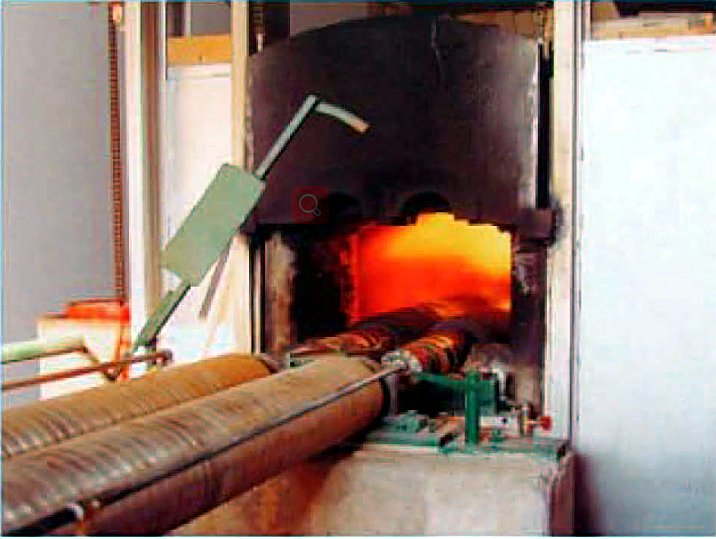
Large fully-automatic centrifugal furnaces cast the 2–5 mm bimetallic alloy layer, with Fuji (Japan) temperature control.
Controlled gas nitriding to HV 900–1020 with a 0.5–0.8 mm case depth, batch-traceable.
Barrel bores machined with German tooling, then honed for diameter and straightness.
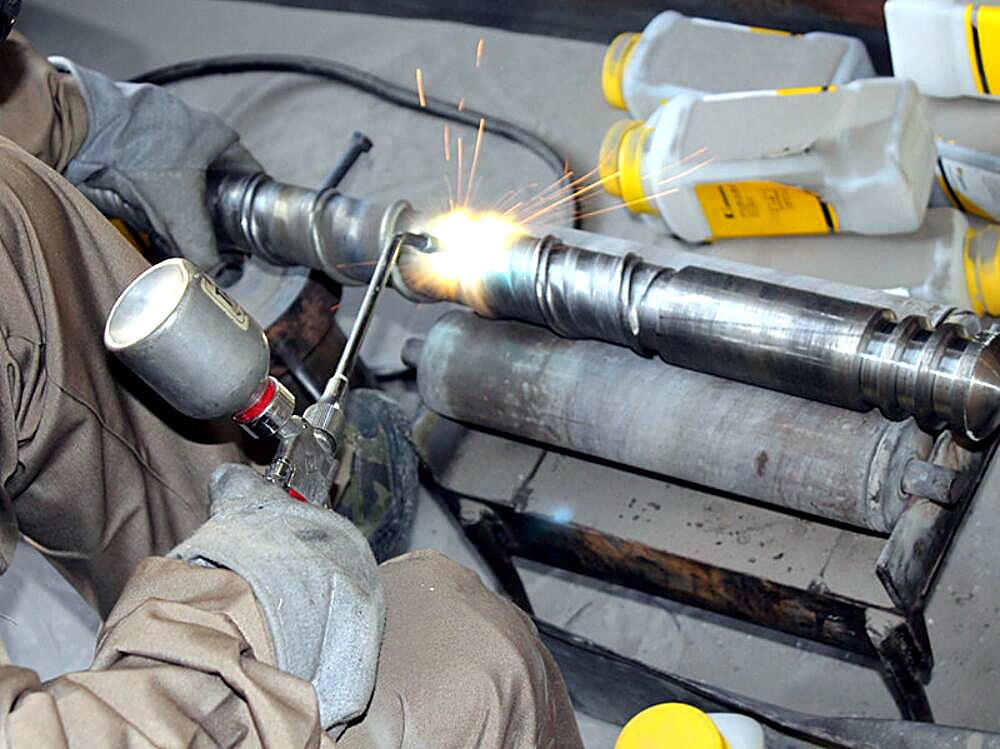
Flight profiles, match marks and fittings machined on CNC equipment to drawing.
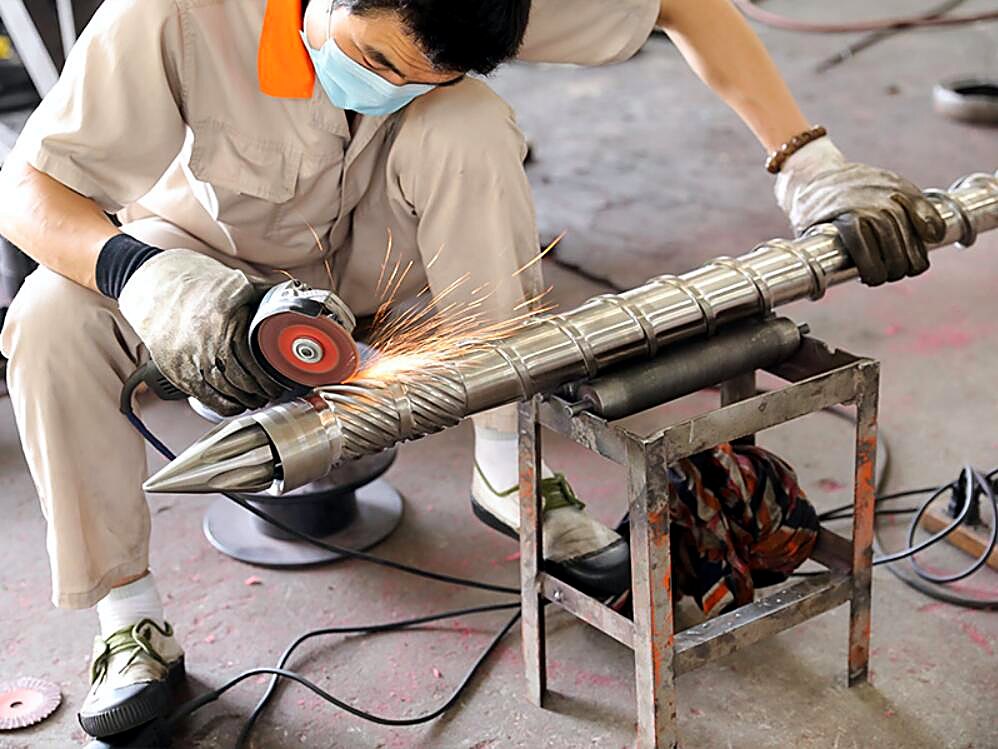
Outer diameter grinding and flight polishing for smooth, accurate profiles.
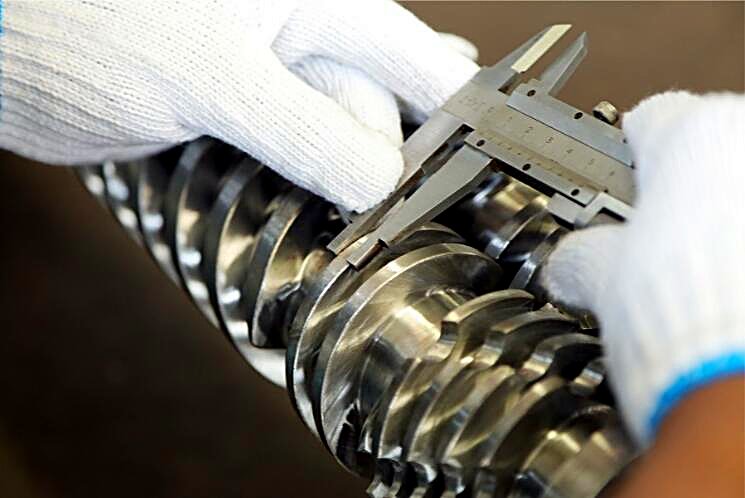
Hardness testers, bore gauges and alignment checks on every finished set before packing.
Certified 38CrMoAlA and alloy steels, spectral-verified per batch.
Bimetallic layer centrifugally cast or bore gas-nitrided.
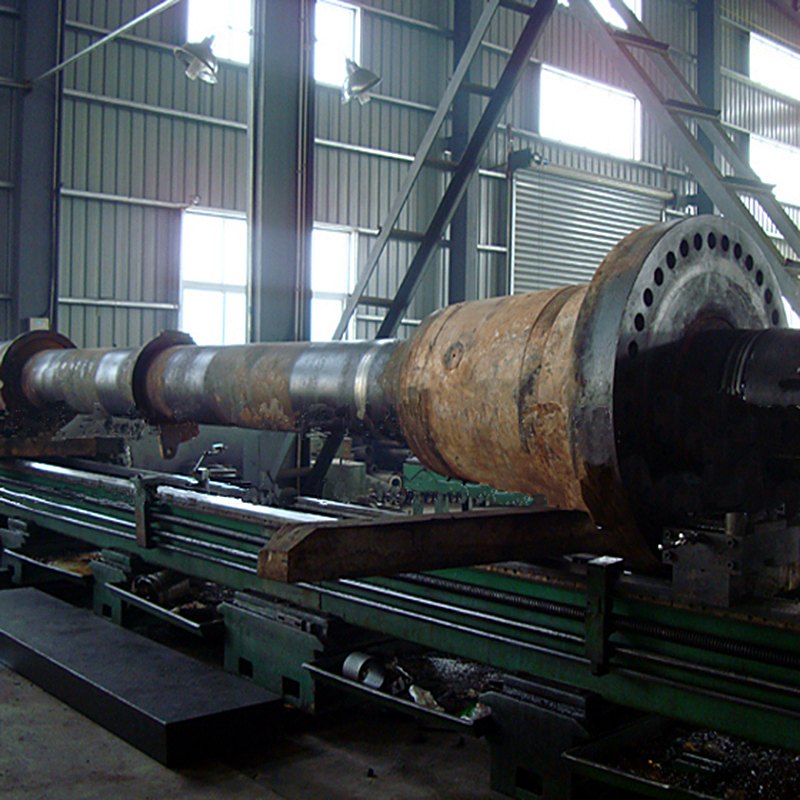
Blank turning, deep-hole boring and honing of the barrel bore.
Flight milling, OD grinding and polishing to final tolerance.
Screw fitted into barrel, clearance and runout recorded.
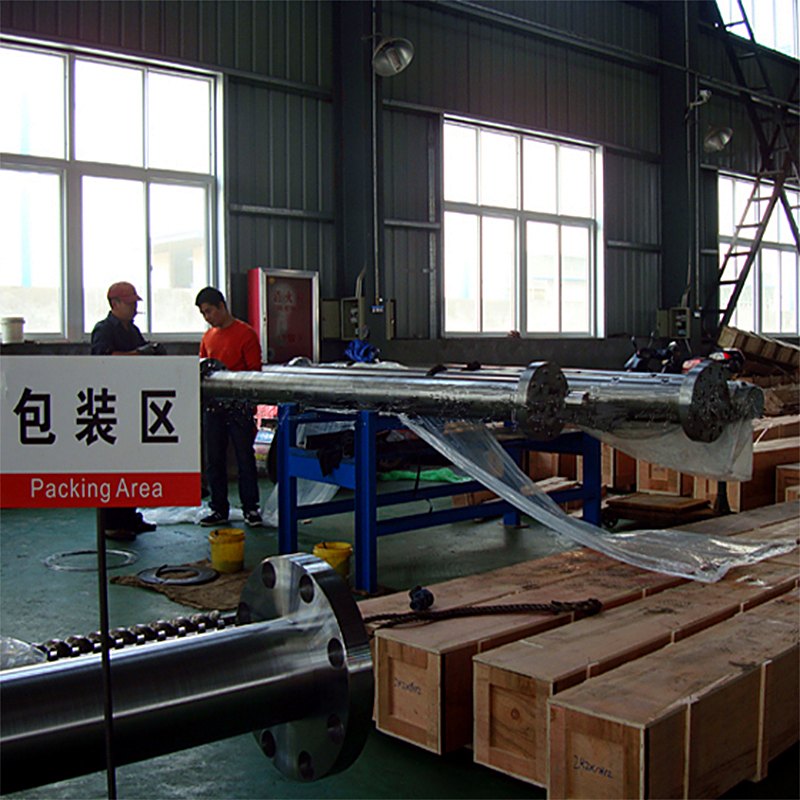
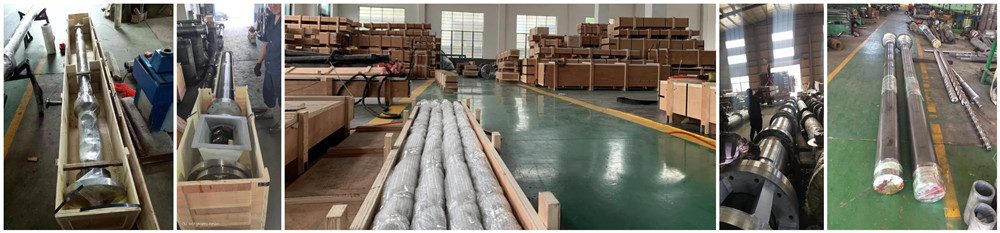
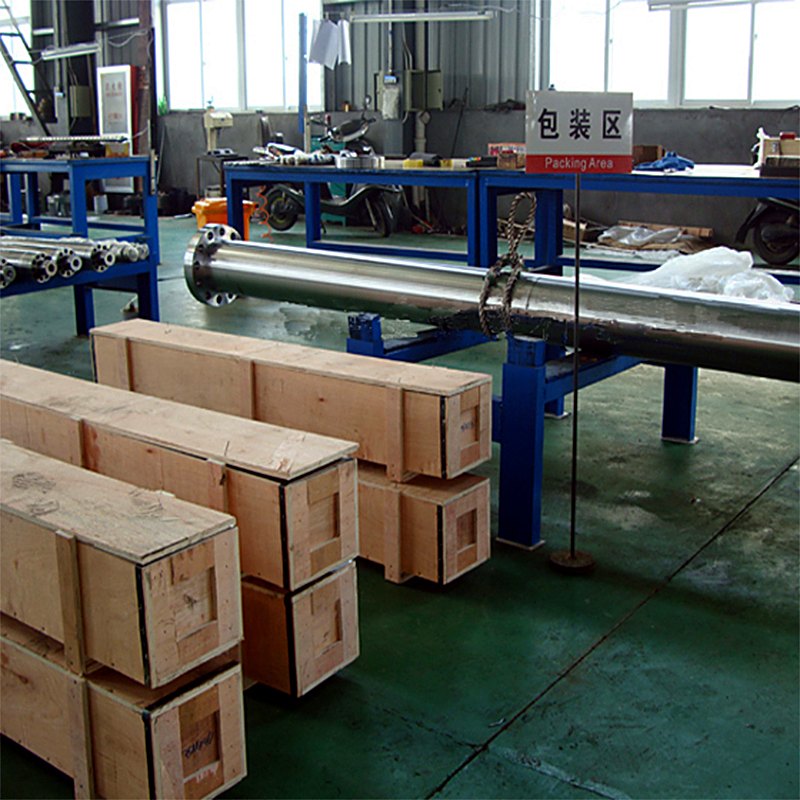
Rust-proofed, capped, wooden-cased and photographed.